METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
‹ › You already have product drawings for Omega profiles and have decided to set up a production line, but you're still not sure how to configure the punching and cutting stations. Can the punching molds be made to your drawings? Should cutting happen before or after forming? Until these questions are settled, the whole…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
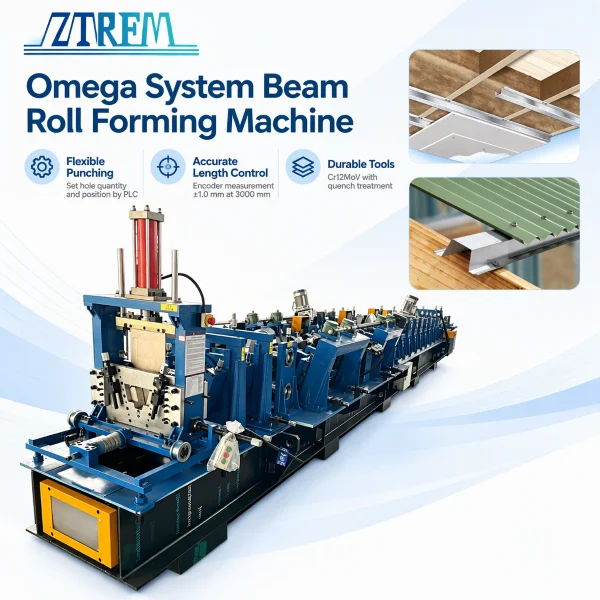
You already have product drawings for Omega profiles and have decided to set up a production line, but you're still not sure how to configure the punching and cutting stations. Can the punching molds be made to your drawings? Should cutting happen before or after forming? Until these questions are settled, the whole line plan can't be finalized. The punching and cutting setup on an omega system beam roll forming machine depends on product cross section, hole positions, finished length, and process sequence.
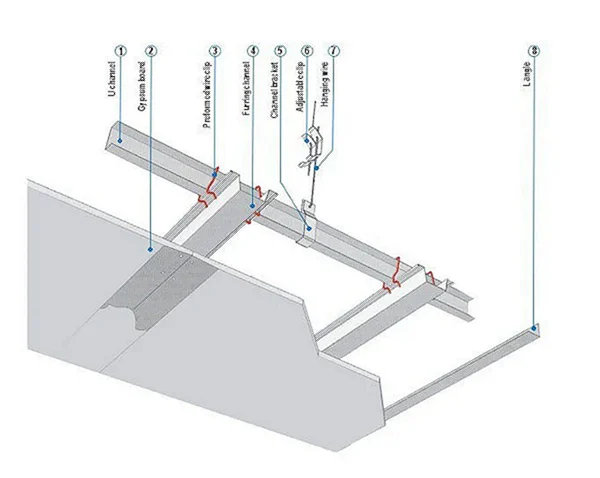
Omega profiles are commonly used in building and industrial sectors. Applications often cited include ceiling and partition systems, light gauge buildings and prefab houses, steel structure purlins and supports, and industrial shelving and storage. These applications are often evaluated on an omega system beam roll forming machine, but specific suitability needs to be confirmed against product drawings and the machine configuration.
In ceiling and partition work, a metal furring studs machine may be considered for furring profiles with wide hole spacing and fixed length production, but the actual product match needs confirmation.
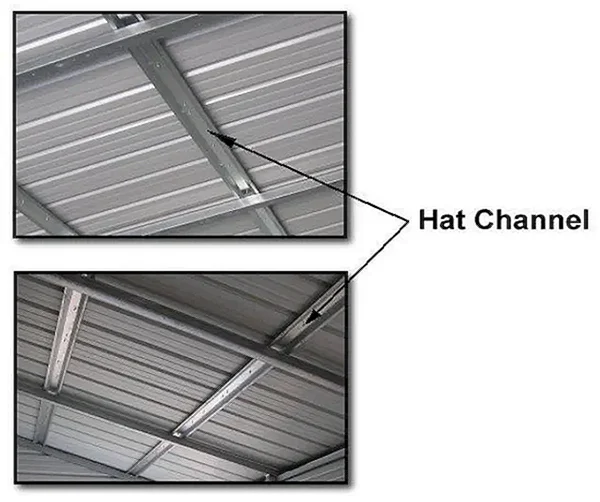
The current omega system beam roll forming machine handles galvanized steel and cold rolled steel, 0.8 to 2.0 mm thick, strength within 440 MPa, with a typical Hat Profile section of 40 mm web and 26 mm flange. Actual product suitability needs to be confirmed.
The following parameters relate directly to punching and cutting:
| Parameter | Current Configuration |
|---|---|
| Processing material | Galvanized steel, cold rolled steel |
| Material thickness | 0.8 to 2.0 mm |
| Material strength | Within 440 MPa |
| Forming stations | 16 stations |
| Punching type | Pre punching (stop punching before forming) |
| Punching mold | Cr12MoV with quench treatment |
| Cutting type | Stop cutting after forming |
| Cutting blade | Cr12MoV with quench treatment |
| Hydraulic stations | 3 sets (2 for punching, 1 for shearing) |
| Length tolerance | 3000 mm ±1.0 mm |
| Working speed | 0 to 30 m/min (depends on hole quantity) |
| Control | PLC touch screen and Omron encoder |
| Voltage | 415 V 50 Hz 3 phase (customizable) |
These are the values for the current configuration on an omega system beam roll forming machine. Voltage can be customized for the target market. Whether other parameters can be customized depends on the specific project.
On an omega system beam roll forming machine, the punching and cutting setup provides several practical points:
Punching is completed on the flat strip, which provides a position reference before forming. Final hole positions still depend on feeding, material flow, and roll forming pass design.
Punching molds and cutting blades use Cr12MoV with quench treatment, selected for wear resistance under their respective working conditions. Actual tool life depends on material, hole pattern, batch size, and operating conditions.
The encoder takes part in length measurement. Under the stated 3000 mm length condition, the length tolerance is stated as ±1.0 mm. Other length conditions need separate confirmation.
Three hydraulic stations are arranged as two for punching and one for shearing. This is a configuration description and does not by itself imply independent operation or optimized rhythm.
The PLC touch screen allows operators to set hole quantity and position, and the system executes to those settings.
These configuration points affect how the punching and cutting setup can be matched to product drawings.
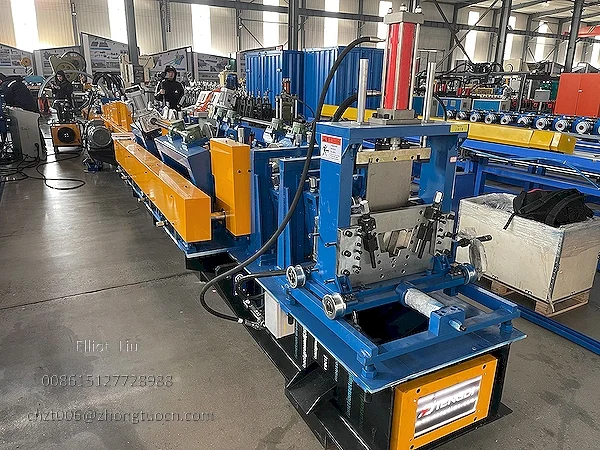
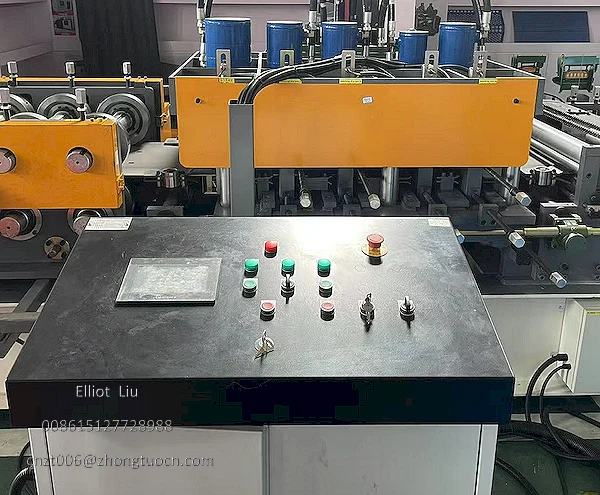
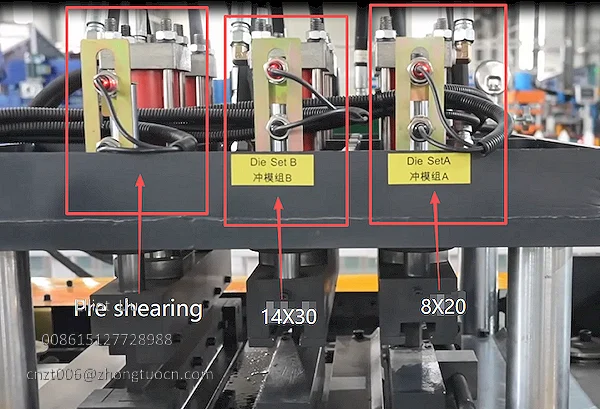
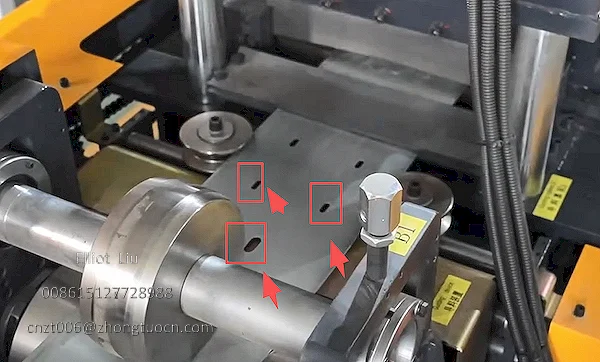
On an omega system beam roll forming machine, punching is completed before forming. Hole positions on the flat strip are determined by the punching mold and feeding action together. Roll forming pass design then determines how material flows during forming, which changes the relative position of holes on the formed cross section. Punching molds and roll forming pass design therefore need to be confirmed together.
Punching mold design for a sheet metal forming omega machine project starts from product drawings: hole type, hole diameter, hole spacing, and hole position. The current machine uses Cr12MoV with quench treatment for punching molds and comes with two standard punching mold types. Punching is configured according to customer drawings.
Items to confirm for custom projects:
Complete product drawings, including section dimensions, hole type, hole spacing, and hole position
Whether the roll forming pass design covers the target section
The punching position before forming and how material flow affects hole positions in practice
On an omega system beam roll forming machine, flat die cutting and profile die cutting work on different objects and have different blade requirements. Flat die cutting completes the cut while material is still flat, with a simple blade shape and a flat cut surface. Profile die cutting completes the cut after forming, with a blade shape that needs to match the Hat Profile section and a cut surface that follows the formed section.
On this omega system beam roll forming machine, the current configuration is stop cutting after forming. An encoder measures length and triggers cutting when the set value is reached. The stated length tolerance is 3000 mm ±1.0 mm for that length condition; tolerances for other finished lengths or working conditions need to be confirmed. The cutting blade uses Cr12MoV with quench treatment.
The cutting method needs to be judged together with product section, cut edge requirements, finished length, production pace, and actual machine configuration. When product length is fixed and batch size is large, cutting after forming may match a continuous production rhythm, but this needs confirmation for the specific product.
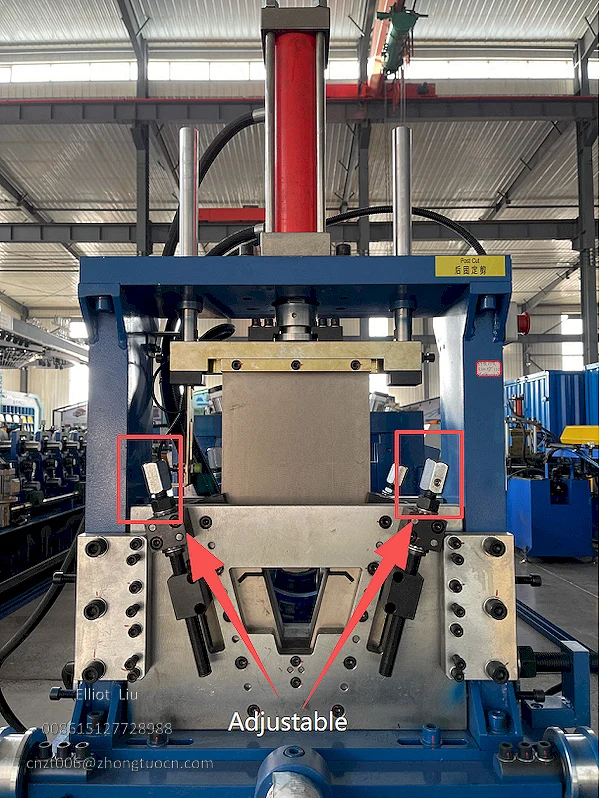
For Omega profiles with holes, the punching and cutting setup needs to be confirmed around product drawings, hole requirements, finished length, and batch size. Whether the punching molds follow the drawings, whether roll forming pass design coordinates with punching, and whether the cutting method matches finished length all affect line performance. The value of an omega system beam roll forming machine ultimately shows in how well the punching and cutting setup matches product requirements.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.