METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
‹ › Many buyers ask about main motor power and hydraulic station count first when buying an omega keel roll forming machine. But after getting those numbers, they still aren't sure if the machine fits their production rhythm. The reason is simple: power and pump station count are only part of the setup. What really shapes…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
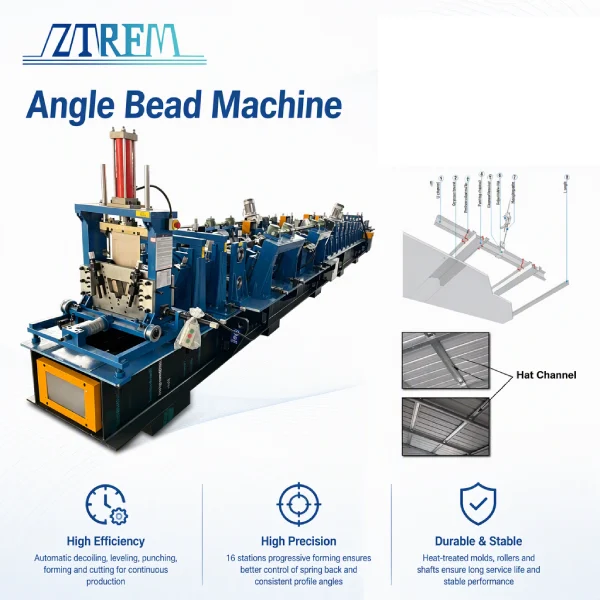
Many buyers ask about main motor power and hydraulic station count first when buying an omega keel roll forming machine. But after getting those numbers, they still aren't sure if the machine fits their production rhythm. The reason is simple: power and pump station count are only part of the setup. What really shapes production performance is how hydraulic power is distributed between punching and cutting, what tasks the main motor and hydraulic system each handle, and whether these settings can be adjusted to match actual production needs. A good machine should be evaluated around specific processing tasks.
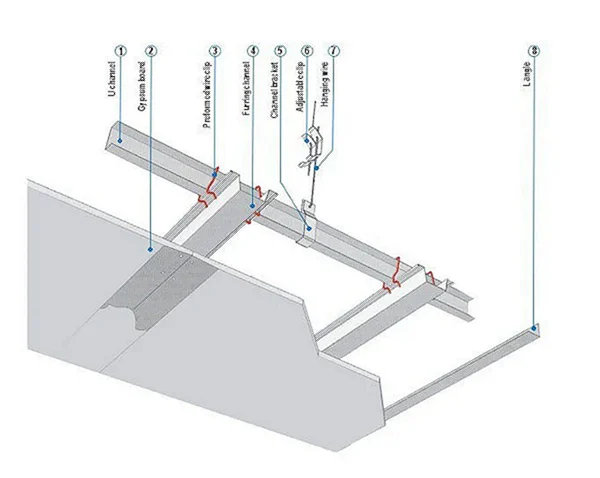
On an omega keel roll forming machine, Omega Keel profiles are widely used in ceiling furring systems, light gauge partition and framing systems, and other building applications. Different applications place different demands on the power setup:
Ceiling furring systems: product lengths are fairly fixed, holes are mainly for installation, and punching frequency is moderate
Light gauge partition and framing systems: more profile sizes and more frequent size changes
Products with dense holes: the punching station has higher requirements for stable hydraulic power
Products with thicker material: the forming station has higher requirements for main motor power
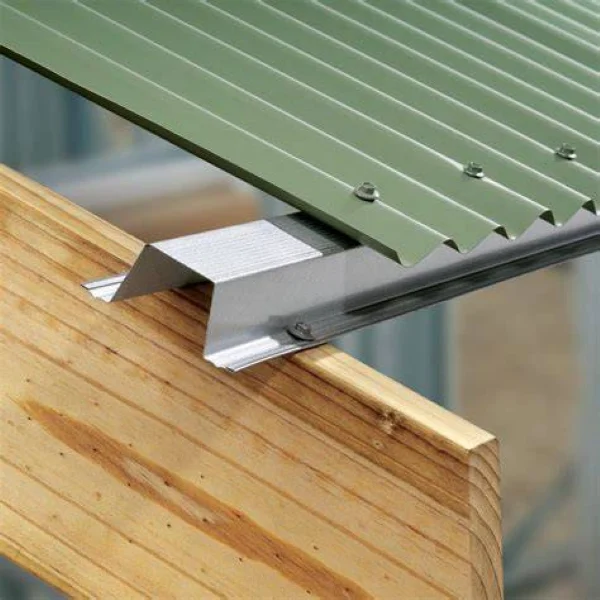
This machine handles galvanized steel and cold rolled steel, material thickness from 0.8 to 2.0mm, and material strength within 440Mpa. The typical profile is an Omega Purlin with a 40mm web and 26mm flange. Specific dimensions can be customized based on customer drawings.
Application scenarios determine what to focus on for power configuration. The setup for an omega profile light keel roll forming machine needs to be confirmed based on actual product requirements.
The following parameters are directly related to the power and hydraulic setup on an omega keel roll forming machine:
| Parameter | Current Configuration |
|---|---|
| Main motor power | 14kw |
| Hydraulic power | 7.5kw |
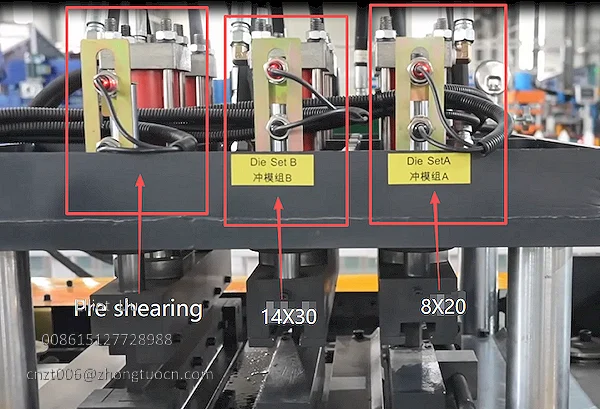
| Hydraulic stations | 3 sets (2 for punching, 1 for shearing) |
| Punching type | Pre punching (stop punching before forming) |
| Cutting type | After forming stop cutting |
| Voltage | 415V 50Hz 3 phase |
| Working speed | 0 to 30m/min (depends on holes quantity) |
| Forming stations | 16 stations |
| Processing material | Galvanized steel, cold rolled steel |
| Material thickness | 0.8 to 2.0mm |
| Material strength | Within 440Mpa |
These are the values for the current configuration. Voltage can be customized for the target market.
Hydraulic stations divided by process: 3 hydraulic stations serve punching and shearing separately on this omega keel roll forming machine, matching the different working rhythms of the two processes
Voltage customizable for target markets: 415V 50Hz 3 phase is the current setting, and it can be adjusted to meet the voltage standards of different export markets
Processes connected in sequence: decoiling, leveling, punching, forming, and cutting run in order to form a continuous production flow
Speed range covers different production rhythms: the 0 to 30m/min working speed range can be adjusted based on actual hole quantity
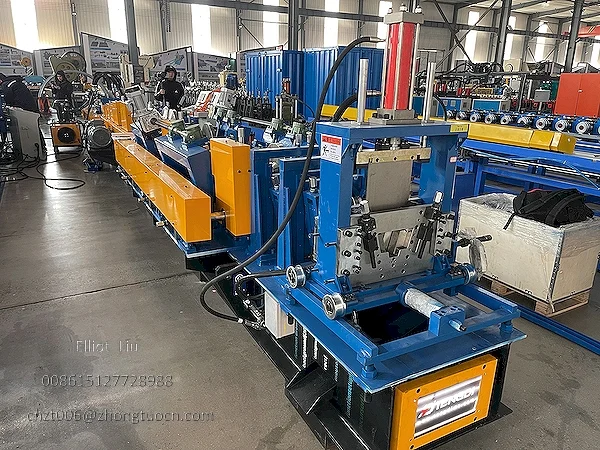
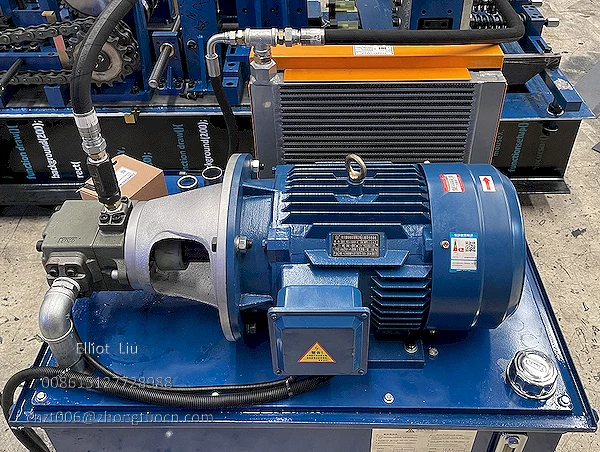
This omega purlin roll foming machine uses 3 hydraulic stations. Two are for punching and one is for shearing. Punching is a high frequency action, with one punching cycle per hole. Shearing is a low frequency action, with one cut per product length. Separating the hydraulic stations accounts for the different working rhythms of the two processes, giving each a relatively stable power output. Hydraulic power is controlled through solenoid valves. Hydraulic power is 7.5kw, using 46# hydraulic oil.
The specific hydraulic station setup on an omega keel roll forming machine needs to be confirmed based on actual production requirements and product specifications.
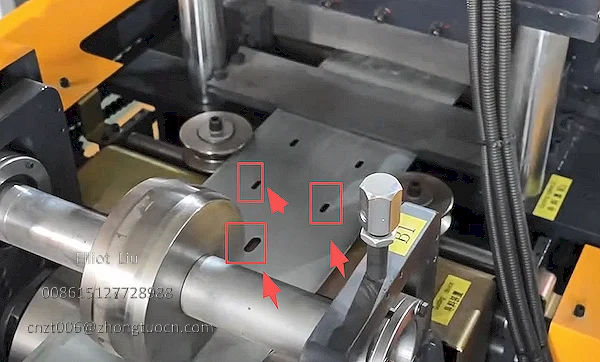
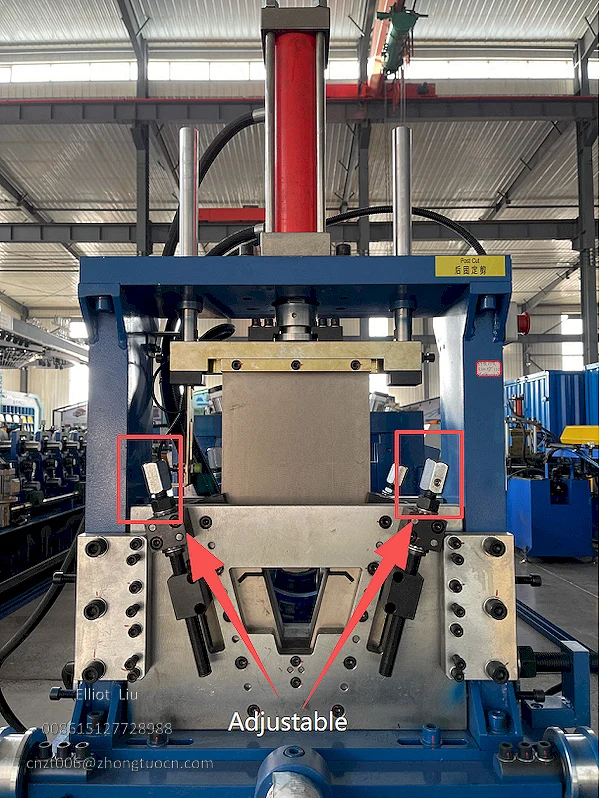
On an omega keel roll forming machine, the main motor drives the forming machine and turns the rollers across 16 stations. Power needs to match material thickness, strength, and forming stations. The hydraulic system drives punching and cutting, which is a different task from the main motor. The main motor handles power output for forming, while the hydraulic system handles power output for punching and cutting. The two need to match but cannot replace each other.
The working speed range is 0 to 30m/min, and actual speed depends on hole quantity and other production conditions. It cannot be judged by main motor power alone. Actual line speed is affected by process actions, machine structure, control rhythm, and operating conditions.
The logic behind power configuration: main motor power is set based on forming needs, and hydraulic power is set based on punching and shearing needs. Both need to be confirmed based on product hole pattern, material thickness, and production batch. Higher power isn't always better. The right match matters more on an omega keel roll forming machine.
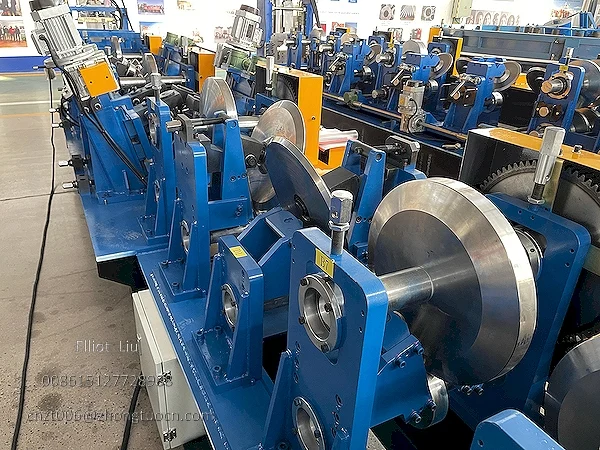
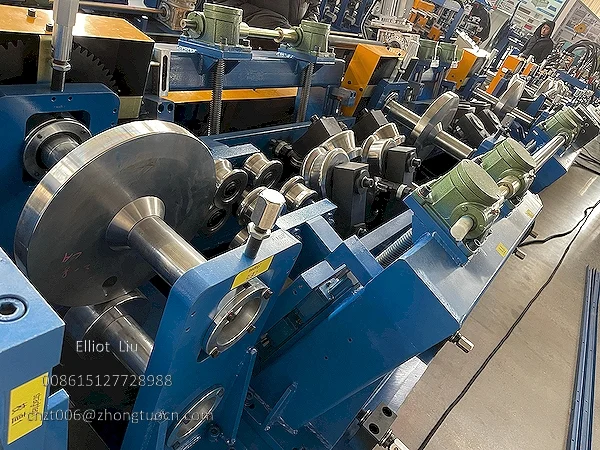
The value of an omega keel roll forming machine ultimately shows in how well the power configuration matches actual production needs. We recommend confirming whether the power setup matches your long term production needs based on your actual product specifications, hole requirements, material thickness, and output targets.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.