METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
‹ › Buying a cold roll forming line is not like ordering a standard machine off a shelf. You are choosing a production line that has to run your profile, at your speed, in your shop, day after day. The questions behind the order are always the same: will it make my C section consistently,…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
Buying a cold roll forming line is not like ordering a standard machine off a shelf. You are choosing a production line that has to run your profile, at your speed, in your shop, day after day. The questions behind the order are always the same: will it make my C section consistently, can it switch profiles without a major tooling bill, and will it land in my plant ready to run. A C profile strut channel roll forming machine built for this class of work answers those questions through its station layout, drive type and control setup. Below is the full line station by station, the typical applications of the finished C section, and the line's configuration.
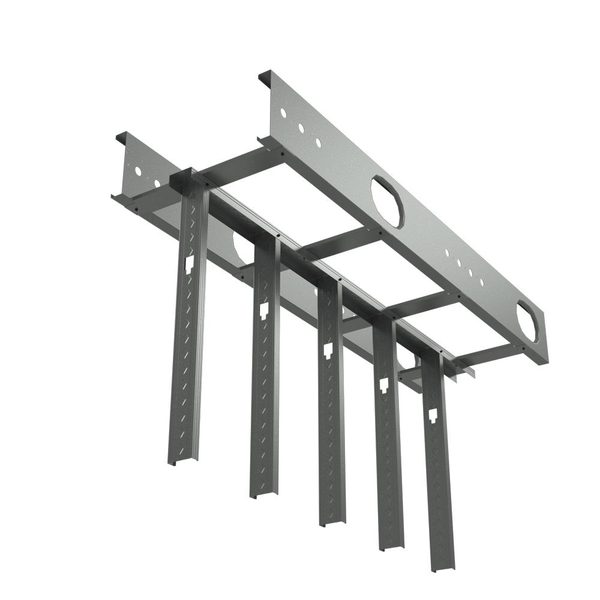
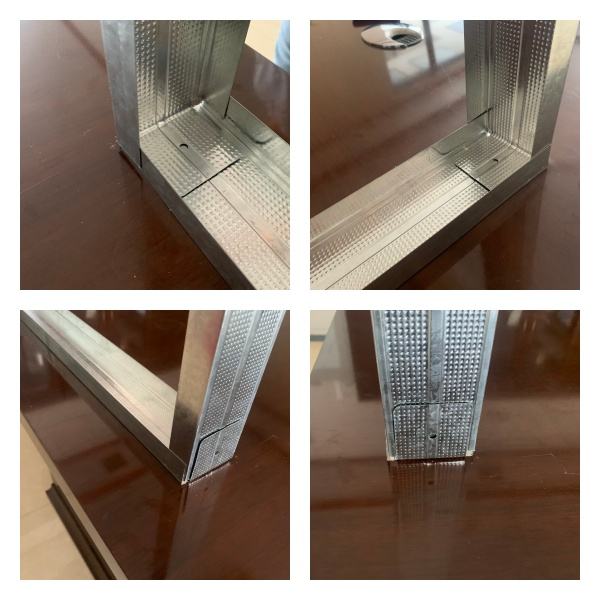
C strut channel is an open cold formed section with a C profile, often embossed on the web or punched with holes. It carries hanging, supporting and connecting loads in light steel structures. Typical configuration covers profile widths around 63.5 mm and 92 mm, with cut lengths around 406 mm and 610 mm.
Profile width, cut length and hole pattern are matched to the project rather than fixed to one size. In North American and Southeast Asian projects, these C sections are widely used as bridging and tie members, and the same equipment is also referred to as a bridging bar roll forming machine.

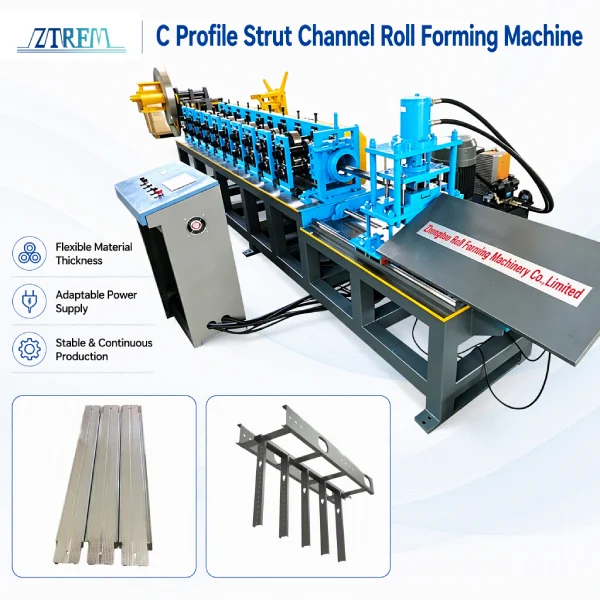
The line runs left to right through six main sections: decoiler, entry guide and leveling, online punching, roll forming, hydraulic flying cut off, and run out table. Each section affects finished profile quality, which is why buyers ask what a C profile strut channel roll forming machine does station by station.
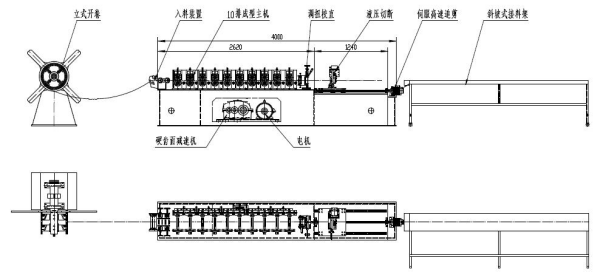
Decoiler. A passive turntable uncoiler sits at the entry. The decoiler is rated for 2.5 ton loading, 300 mm strip width, and 450 to 550 mm coil ID. The coil rests on the turntable and is pulled by the main line rather than driven. Loading capacity, width and ID range are matched to the customer coils.
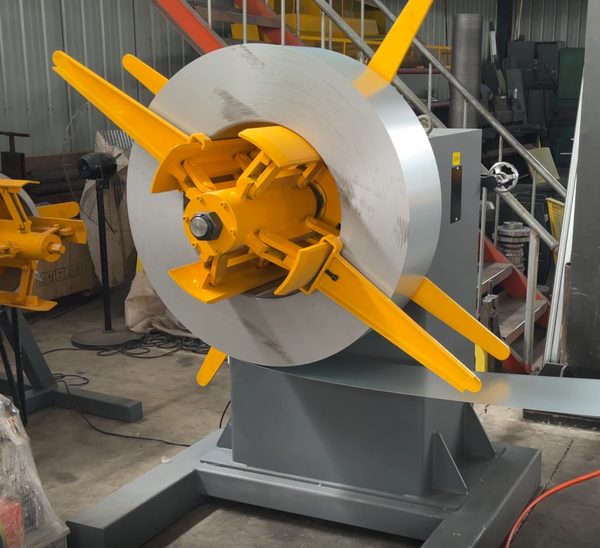
Entry guide and leveling. Strip leaves the decoiler through the entry guide and leveling section. Coil curve and edge wave are flattened and centered before forming. This first section determines whether strip runs straight.
Online punching. Holes are punched either before or during forming, per the drawing. Punching runs off the hydraulic station and remains synchronized with line speed.
Roll forming. Flat strip passes through 12 forming stations in this configuration. Each station bends the sheet incrementally until the full C section is formed. Station count varies with profile complexity. Forming rolls are GCr12, polished, hard plated and heat treated. Shafts are 45# tempered steel around 50 mm diameter.
Hydraulic flying cut off. At set length, a hydraulic blade descends. The blade is Cr12 quenched and driven by a servo motor. The cut off follows line speed and cuts on the fly without stopping the line. Blade material and hydraulic power are matched to strip thickness and cut force.
Run out table. Cut pieces slide down a 3 m receiving table and are stacked by hand or automatically.
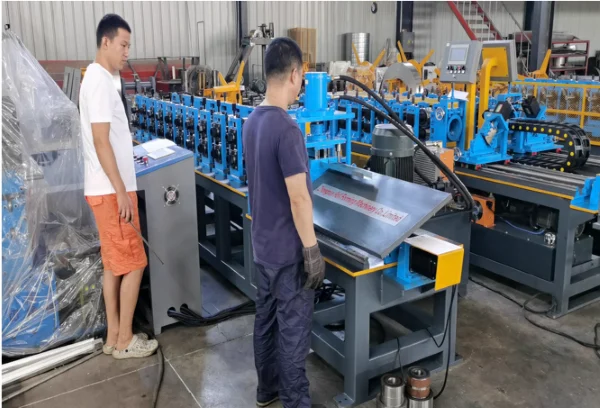
Line speed is 0 to 15 m per minute with punching and cut off. Actual speed is set by profile complexity and output target.
Beyond the basic station sequence, a C profile strut channel roll forming machine built for this configuration is designed as an integrated line rather than a collection of separate machines. The decoiler, forming stations, punching, flying cut off and run out table are synchronized through one PLC, so the operator sets length and piece count once and the whole line follows.
Multi profile changeover without new tooling. Width is changed by adjusting roll spacers rather than machining a new roll set. The line runs two profile widths, around 63.5 mm and 92 mm, on the same setup. If future projects add a third width, the same spacer adjustment logic applies rather than buying a second machine.
Online punching and flying cut off without stopping the line. Punching runs off the hydraulic station in sync with line speed. The servo driven cut off follows the strip and cuts on the fly, so the line does not pause between pieces. This matters more on short cut lengths like 406 mm and 610 mm, where stop and go cutting would waste cycle time.
Forming rolls built for galvanized strip contact. Rolls are GCr12, polished, hard plated and heat treated. Shafts are 45# tempered steel around 50 mm diameter. The surface treatment is specified because galvanized strip can gall on unfinished rolls, and the heat treatment keeps the roll profile stable over long runs.
One touch screen for the whole line. PLC, inverter and touch panel are integrated. Operators set length, piece count and speed on the panel, and the machine counts and cuts automatically. The screen supports English and Chinese, which reduces training time for overseas crew.
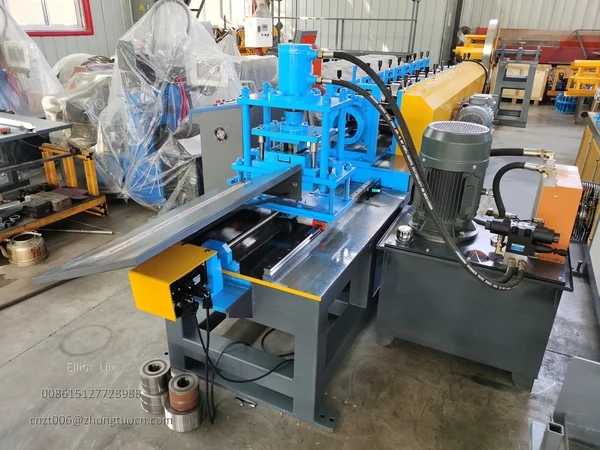
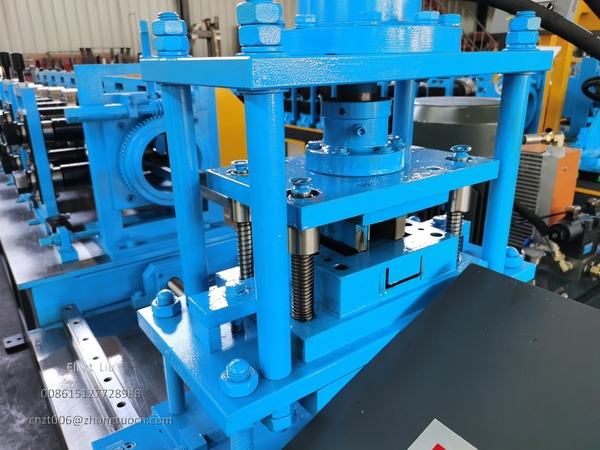
The table below lists the typical configuration for a C profile strut channel roll forming machine, not an industry standard. Strip thickness, width, station count, speed, motor power, voltage, drive type and decoiler capacity are all matched to the project.
| Item | Typical configuration |
|---|---|
| Material | Galvanized steel, thickness band around 0.35 mm to 0.45 mm |
| Forming stations | 12, adjusted by profile complexity |
| Line speed | 0 to 15 m per minute with punching and cut off |
| Punching | Online hydraulic, hole pattern per drawing |
| Cut off | Hydraulic servo flying cut off, Cr12 quenched blade |
| Main motor | 5.5 kW |
| Hydraulic station | 7.5 kW, #46 hydraulic oil |
| Control | PLC plus inverter plus touch screen, English and Chinese |
| Voltage | 480 V 60 Hz three phase, adjustable to destination |
| Decoiler | 2.5 ton loading, passive uncoil |
| Machine weight | Around 5.5 tons |
| Footprint | Around 12 m by 2.0 m by 1.5 m including run out |
Voltage matters for overseas buyers. If the shop operates on 415 V 50 Hz or another grid, the voltage, phase and frequency should be confirmed before order. Control and motor configurations can be built to the local grid.
The product range also covers adjacent open and closed section lines, including C purlin machines, light steel keel machines, cable tray lines and guardrail lines. Tooling and cut off can be matched to separate drawings.
If your profile drawing, strip thickness and shop voltage are already defined, send them over. A C profile strut channel roll forming machine can be configured to match the project rather than delivered as a fixed standard unit.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.