METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
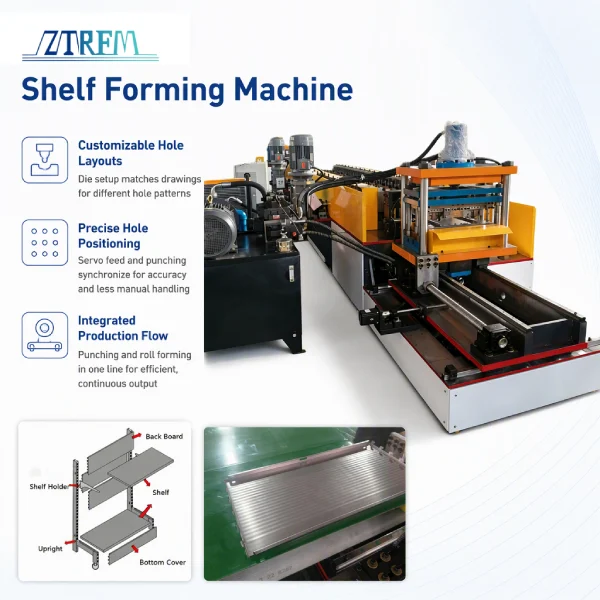
‹ › Hole processing for rack back panels is a key step. Different rack systems need different hole patterns, sizes, and layouts. A shelf forming machine matches the right punching die setup and connects punching, edge trimming, and forming in continuous production. Rack Back Panel Hole Pattern Applications and Needs Storage racks: panels need specific hole designs…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
Hole processing for rack back panels is a key step. Different rack systems need different hole patterns, sizes, and layouts. A shelf forming machine matches the right punching die setup and connects punching, edge trimming, and forming in continuous production.
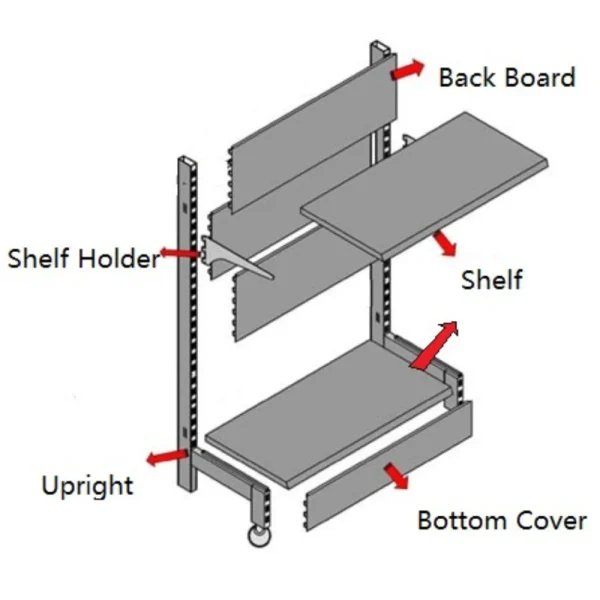
Storage racks: panels need specific hole designs from the customer drawing
Supermarket shelving: panels support display and mounting needs
Mezzanine and industrial racks: panels need specific profiles and hole positions
A shelf back panel machine handles these variations based on the confirmed drawing.
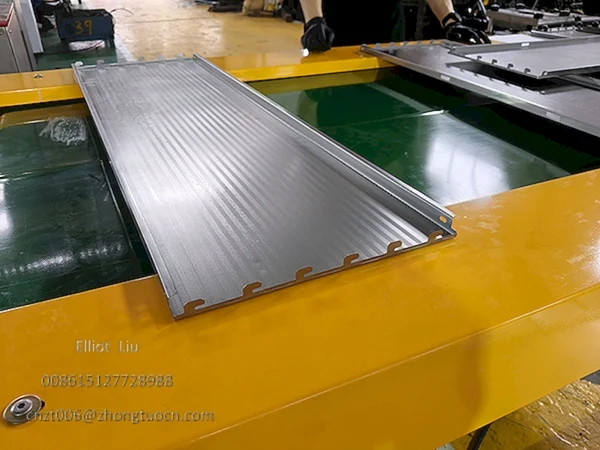
Punching dies determine the hole pattern. A shelf forming machine configures its setup to the panel hole drawing. The current setup uses 3 sets of front dies for ear punching and 8 sets of rear dies for holes.
The servo feeder sends the sheet into the punching station at a set pace. Feed accuracy affects hole spacing, but actual accuracy depends on the confirmed solution.
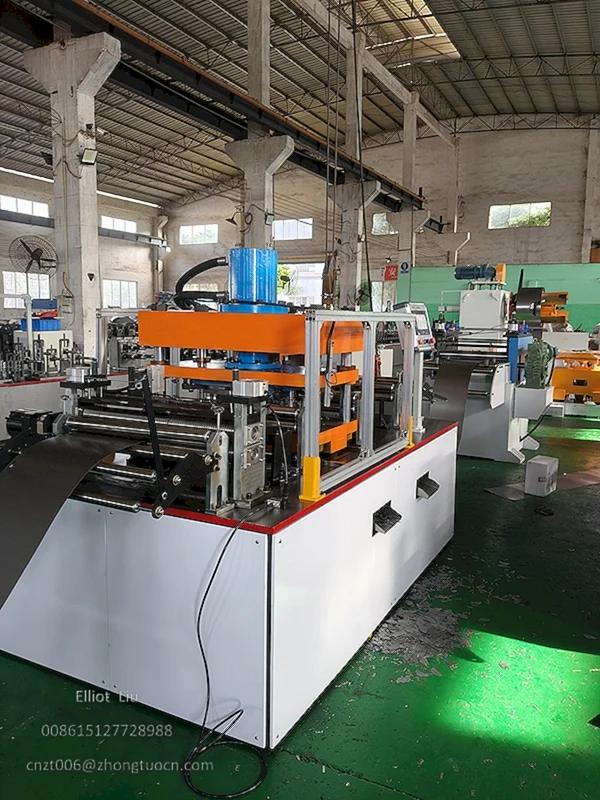
The process runs from decoiling and leveling to servo feeding, punching, roll forming, and cutting. The sheet goes through punching and forming in one continuous feed, reducing handling. Cutting comes after forming.
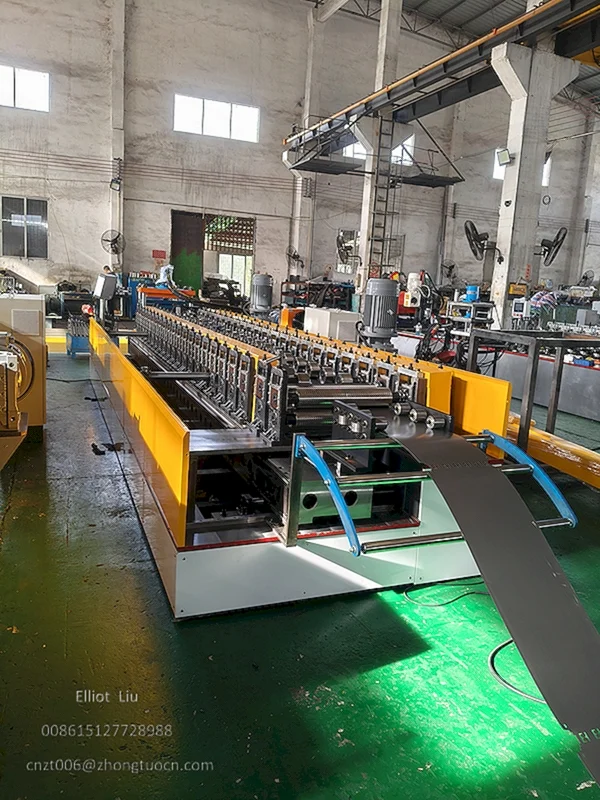
Matching Different Hole Drawings
A shelf back panel machine matches the punching die setup to customer drawings. When a customer makes panels with various hole patterns, the die setup can change.
Hole Position Control in Continuous Production
The servo feed and punching action run at the same pace. This method cuts manual handling. Feed accuracy affects punch position.
Production Value from Process Integration
Putting punching and roll forming on one line cuts waiting between steps. The coil goes in, and the punched panel comes out in a single flow.
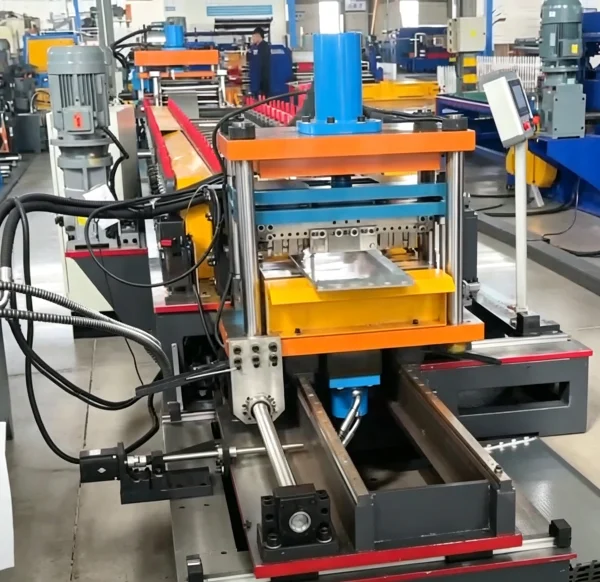
Why Scrap Handling Matters
Continuous punching makes metal scrap. If scrap does not clear in time, it can pile up in the die area and affect production.
Scrap Handling in the Current Solution
The exact scrap collection setup depends on the actual machine configuration. You can discuss this with the maker based on your workshop layout.
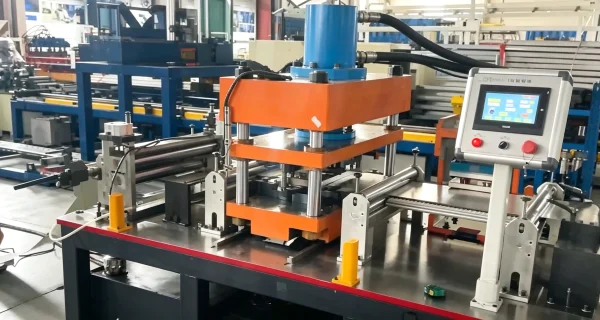
The parameters below come from the current actual solution for a shelf forming machine.
| Item | Specification |
|---|---|
| Raw material | Q235 steel coil |
| Material thickness | 0.4 to 0.8 mm |
| Coil inner diameter | 450 to 550 mm |
| Coil outer diameter | up to 1200 mm |
| Coil weight | 5 tons |
| Forming speed | 0 to 80 m/min (continuous run, cutting stop time not included) |
| Forming width | 99 to 499 mm |
| Punching | 3 sets of front punching dies and 8 sets of rear punching dies |
| Cutting | Hydraulic cutting |
| Total power | 30 KW |
| Main motor | About 15 KW |
| Servo feeder | Huichuan servo motor 1.3 KW, feed speed 15 to 30 m/min |
| Control system | Mitsubishi PLC + Yaskawa or Inovance frequency converter |
| Fault alarms | Material shortage, jams, emergency stop, counting, etc. |
The punching setup is directly related to hole processing. The servo feeder specs relate to feed control.
Send Hole Drawings and Product Needs
Provide the panel hole drawing, hole size, layout, and profile drawing. Also include material thickness, width needs, output target, and changeover frequency.
Maker Review
The maker reviews the punching die setup from the drawing, including front and rear die counts. They give a matched setup and quote.
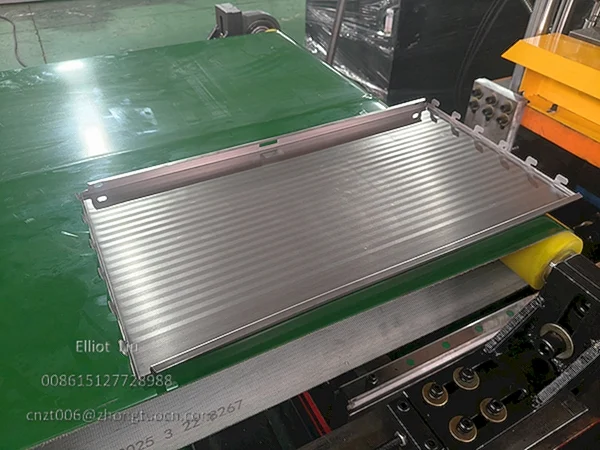
A shelf forming machine follows one core logic: match the punching die setup to the panel hole needs. Different hole drawings need different die plans. Send us your drawing and production needs to confirm a solution.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.