METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
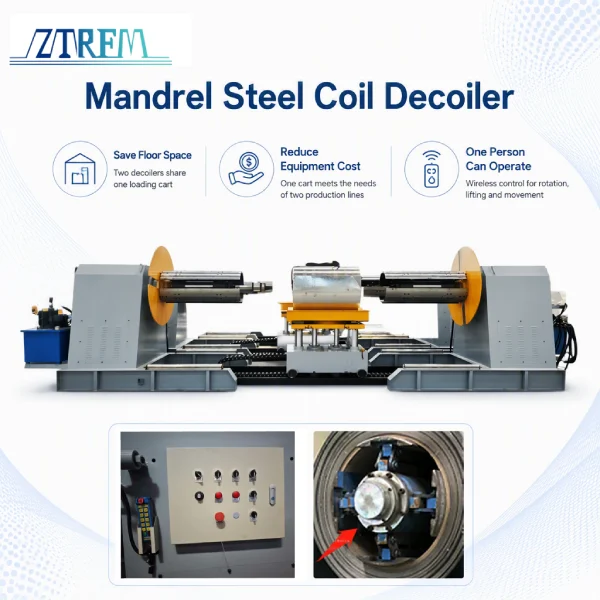
‹ › In a steel coil processing workshop, two independent production lines each need a steady coil supply. If each mandrel steel coil decoiler has its own loading cart, you need two carts instead of one. This machine uses a layout with two decoilers spaced 2 meters apart and sharing one cart track. Each decoiler has its…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
In a steel coil processing workshop, two independent production lines each need a steady coil supply. If each mandrel steel coil decoiler has its own loading cart, you need two carts instead of one. This machine uses a layout with two decoilers spaced 2 meters apart and sharing one cart track. Each decoiler has its own control system and can run independently at the same time. This article also explains how small gear rotation accuracy and same side control cabinets support this setup.
Typical production lines include:
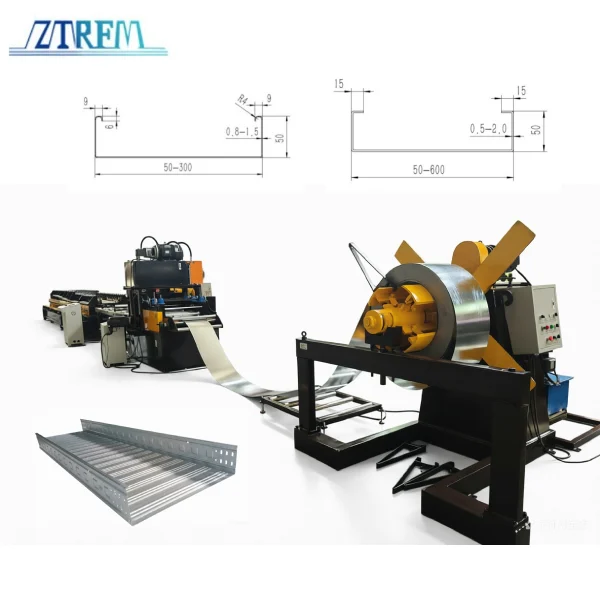
Cable tray production lines
Decorative strip production lines
Steel purlin production lines for C purlin or Z purlin
Solar mount profile production lines
Storage rack production lines
These lines often run two independent forming lines side by side. Each line needs its own coil supply. This is where the two decoiler layout becomes useful.
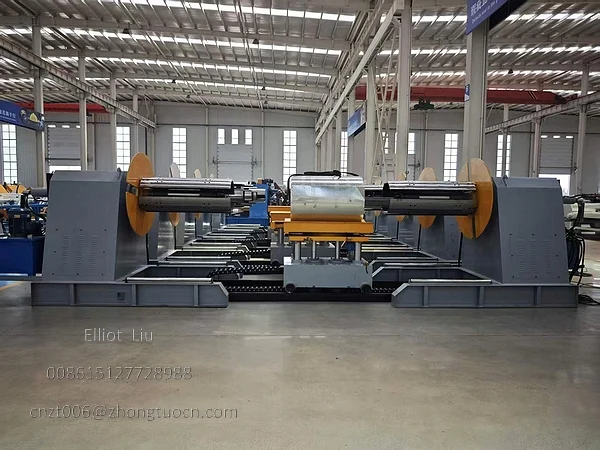
The two decoilers sit 2 meters apart and share one cart track. This distance allows the cart to move between the two machines.
Each mandrel steel coil decoiler has its own control system. The two decoilers can run independently at the same time, each doing uncoiling, expansion, and payoff.
Independent control means each decoiler has its own buttons and remote signal receiver. An operator can start decoiler No.1 alone while decoiler No.2 stays on standby. The two machines don't interfere with each other.
When one line needs a coil change, the operator moves the cart to that decoiler. The other line keeps getting material from its own decoiler.
The cart track runs between the two decoilers. Sharing the track means the two decoilers use a compact layout, and the cart can move between the two stations.
The loading cart is 1250 mm wide, matching the maximum coil width. The cart carries the coil along the track. Once in place, it uses 360 degree electric rotation to adjust its angle and align with the decoiler mandrel.

Both decoilers can control the loading cart separately, but the cart can serve only one decoiler at a time. This is a clear requirement in the product configuration.
The two decoilers run independently. The cart serves one decoiler at a time, so the shared resource has clear rules.
One shared loading cart reduces repeated loading device configuration
Two decoilers use 2 meter spacing for a compact layout
Each decoiler has independent control and can run alone at the same time
The cart serves one decoiler at a time
The accuracy of cart rotation affects how well the steel coil aligns with the decoiler mandrel. If the rotation angle is too far off, the operator has to adjust repeatedly.
This mandrel steel coil decoiler uses a small gear transmission. The quotation states that the small gear ensures rotation accuracy. Motor power goes through the small gear to the rotating platform and drives the cart to adjust its angle.
The loading cart supports 360 degree electric rotation. The small gear structure transfers motor power to the rotating platform and keeps rotation controlled.

The coil inner diameter range is 450 mm to 610 mm. After the cart rotates, the mandrel must enter the coil inner diameter accurately. If the rotation angle is too far off, the mandrel may hit the coil inner ring.
The small gear structure helps the operator adjust the cart angle for alignment.
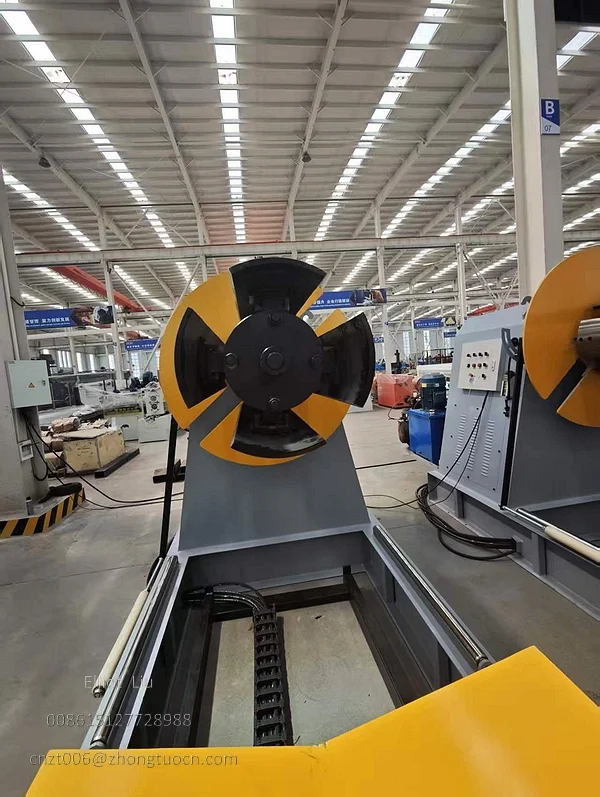
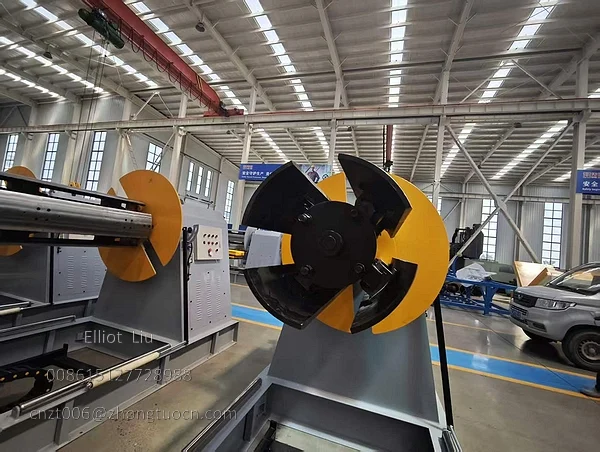
The control cabinets for both decoilers are on the same side of the roll forming machine. Site operation requires both decoiler control cabinets on the same side.
This mandrel steel coil decoiler places both control cabinets on the same side. This is a clear requirement in the product configuration.
Placing the control cabinets on the same side reduces operator movement. During a coil change, the operator does not need to run from one end of the workshop to the other. All control buttons, remote signal receivers, and status displays are in the same area.
The two decoilers have independent control, but the operator needs to observe and operate them in the same production area. If the cabinets are on opposite sides, the operator must walk back and forth.
Same side placement helps centralize operation. The operator can complete loading, uncoiling, and speed control on the forming machine side.
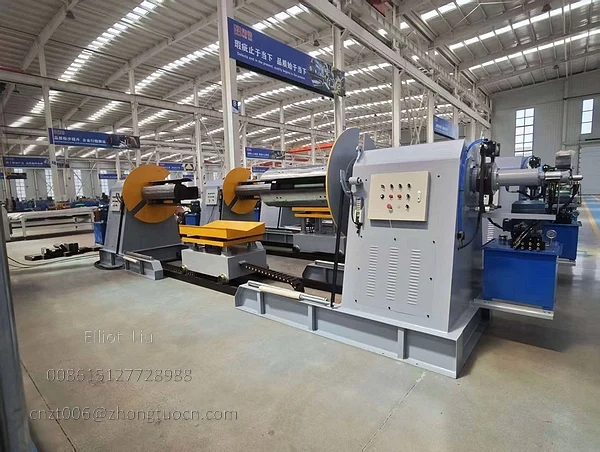
Each decoiler has independent buttons and a remote control. The operator can use local buttons for fine adjustment or use the remote to control rotation, expansion, and payoff start stop from the crane lifting position or beside the cart.
This plc controller decoiler machine includes a control system that manages both decoilers. The quotation lists the control method as local buttons plus wireless remote, and the control panel supports Chinese and English switching.


The following parameters for the mandrel steel coil decoiler are based on the quotation.
| Parameter | Specification |
|---|---|
| Number of decoilers | 2 units, independently controlled |
| Coil inner diameter | 450 mm to 610 mm |
| Coil width | up to 1250 mm |
| Material thickness | 0.4 mm to 1.0 mm |
| Working speed | 0 to 40 meters per minute |
| Hydraulic system power | at least 5.5 kW |
| Drive system power | at least 7.5 kW |
| Loading cart width | 1250 mm |
| Cart rotation | 360 degree electric |
| Decoiler oil cylinder diameter | at least 150 mm |
| Braking system | pneumatic brake |
| Control method | local buttons plus wireless remote |
| Control panel language | Chinese and English |
| Decoiler rotation direction | reversible |
| Distance between two decoilers | 2 meters |
| Power supply | 380 V 50 Hz three phase |
Please confirm the two decoiler spacing, control cabinet side, coil specifications, and power conditions for your project. The automatic speed adjustment for decoiler can be discussed based on your production needs.
This mandrel steel coil decoiler uses a 2 meter spacing dual machine layout, shared cart track, small gear rotation accuracy, and same side control cabinets. It reduces one cart configuration and helps centralize operation of the two decoilers.
Your production line needs two decoilers sharing one cart at 2 meter spacing with control cabinets on the same side. We can confirm the specific configuration based on your coil specifications and site layout. Contact us for a detailed proposal.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.