METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
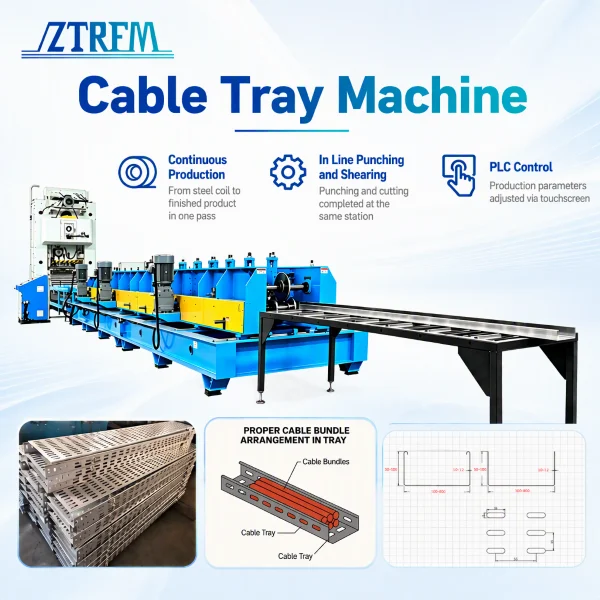
‹ › Punching burr is one of the first quality concerns buyers raise when evaluating a cable tray machine. Excessive burr can affect finished appearance and may complicate later installation and cable routing. It rarely has a single cause. Die condition, material, and equipment status all play a part, so a practical check starts with these…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
Punching burr is one of the first quality concerns buyers raise when evaluating a cable tray machine. Excessive burr can affect finished appearance and may complicate later installation and cable routing. It rarely has a single cause. Die condition, material, and equipment status all play a part, so a practical check starts with these three areas.
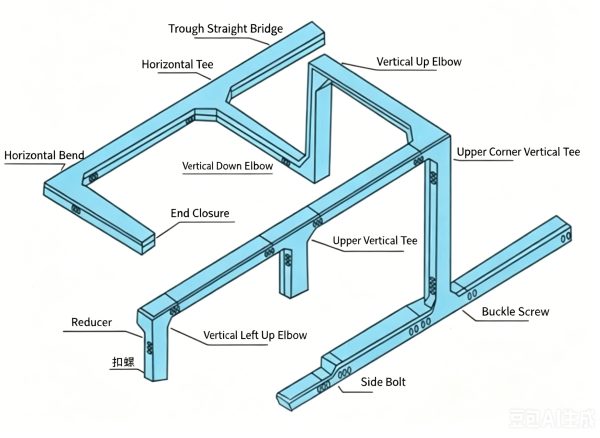
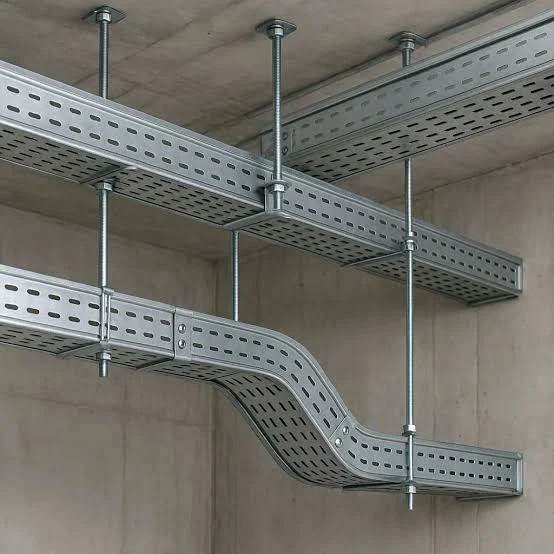
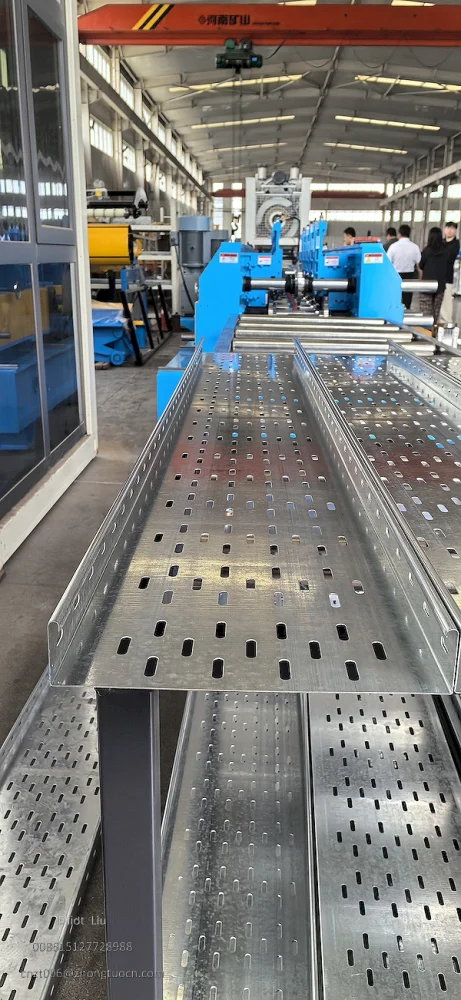
This cable tray machine produces cable tray troughs used to support and protect cables. The products are widely used in the following scenarios:
Data centers: for computer room cable management.
Telecommunication projects: for base station and equipment room cable support.
Industrial plants: for power cable routing in production workshops.
Commercial buildings: for electrical installation in malls, hospitals, and office buildings.
Different projects have different requirements for finished product specifications, hole patterns, hole spacing, and burr quality. A perforated cable tray roll forming machine also needs these details confirmed with the order.
Excessive punching burr is usually not caused by a single factor. Check the die, material, and equipment condition. The following are common influencing factors. For a specific machine, also confirm equipment configuration and die condition.
Clearance between punch and die affects the quality of the cut edge. If clearance is too large, burr may increase, rollover may become more noticeable, and the cut edge may change. If clearance is too small, punching force may rise, die wear may accelerate, and secondary shearing may occur on the cut edge. These effects are not guaranteed to appear in every material and thickness.
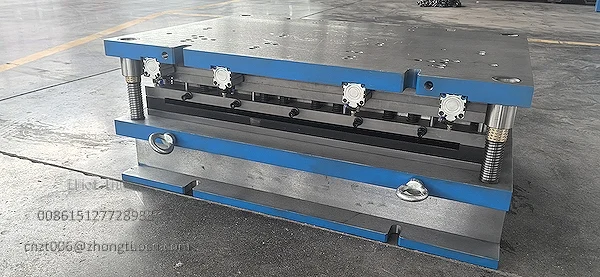
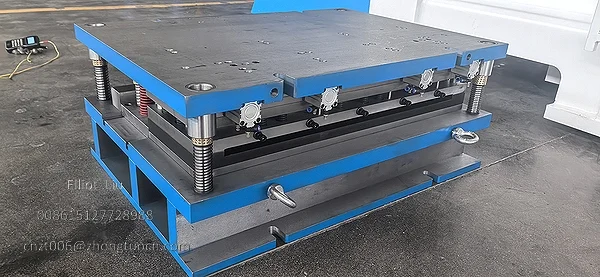
This machine uses a combined punching and shearing die, with punching and cutting integrated at the same station. Actual clearance needs to be determined by material, thickness, die design, and processing requirements.
Die Edge Condition
Die edge wear, chipping, or rough surface may reduce cut edge quality and increase burr. During continuous punching, edge condition changes gradually and needs regular inspection. The maintenance interval depends on punching quantity, material type, and thickness.
Sheet Material and Thickness
Material type and thickness affect deformation and burr formation during punching. For this cable tray machine, the reference materials are Q235B cold rolled strip, hot rolled strip, and galvanized sheet, with a reference thickness range of 1.0 to 1.2 mm.
If the order material or thickness falls outside the current reference range, confirm with the supplier whether the die and punching unit configuration need adjustment.
The following parameters represent a current reference configuration. Speed, voltage, floor space, profile type, and other items can be adjusted to customer order requirements. The exact adjustment range depends on equipment structure and actual configuration.
| Parameter | Specification |
|---|---|
| Processing thickness | 1.0 to 1.2 mm |
| Rolling strip width | 200 to 1050 mm |
| Product specification | 100×50 to 800×100 mm |
| Applicable materials | Q235B cold rolled strip, hot rolled strip, galvanized sheet |
| Production speed | 6 to 10 m/min |
| Length and width tolerance | ±1.5 mm |
| Angle tolerance | 90°±2° |
| Total installed power | Approx. 60 kW |
| Machine dimensions | 35×1.5×1.6 m (L×W×H) |
| Voltage | 380 V, 50 Hz, 3 phase or as required |
| Motor explosion proof rating | ExdICT4 |
| Motor protection rating | IP55 |
These values are a reference configuration, not a general standard for all machines of this type.
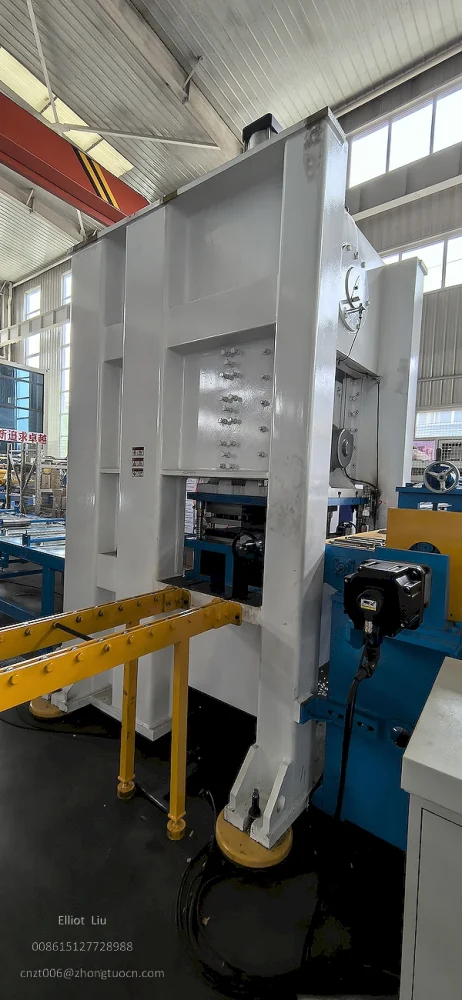
On this cable tray machine, the 200t figure refers to the tonnage of the punching unit, not the whole machine. It does not by itself mean smaller burr, better punching quality, or higher punching accuracy.
The combined punching and shearing die integrates two operations at one station. This affects process flow. Punching quality still depends on die clearance, edge condition, material, thickness, and actual processing conditions.
The servo feeding system handles feed length and position control. It does not directly guarantee hole position accuracy or burr quality.
PLC control coordinates machine actions and production flow. It is not a burr control system.
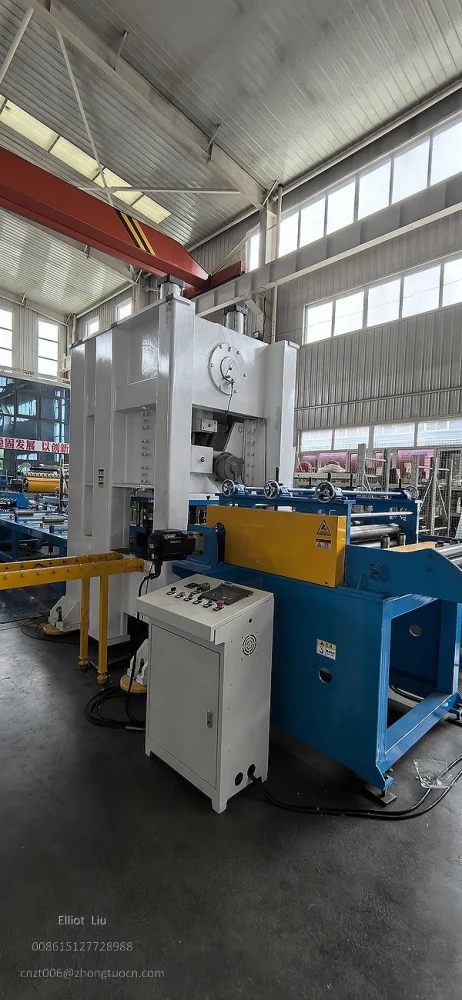
Integrated Punching and Shearing
Two operations run at one station, so the process flow is shorter.
Servo Feeding Control
Feed length and position are controlled for the punching process.
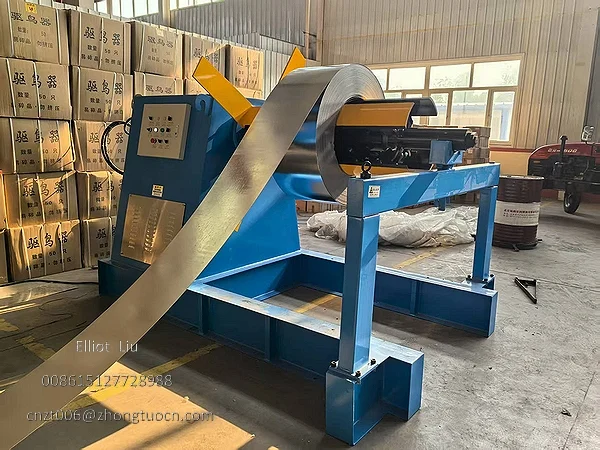
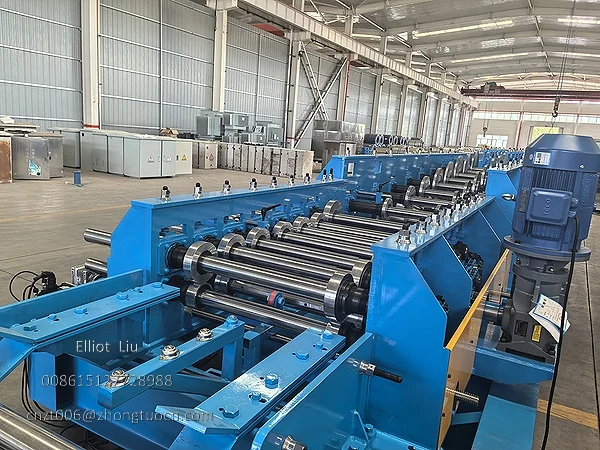
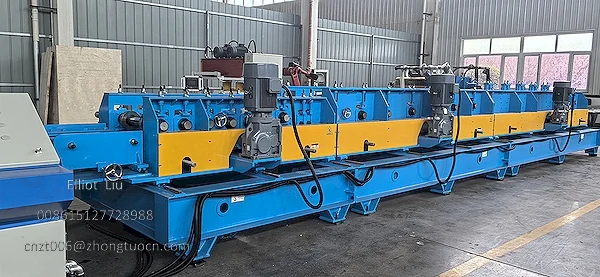
Continuous Production Line
The machine supports a continuous production flow from coil to finished part.
PLC-Based Operation
PLC control coordinates machine actions and production parameters.
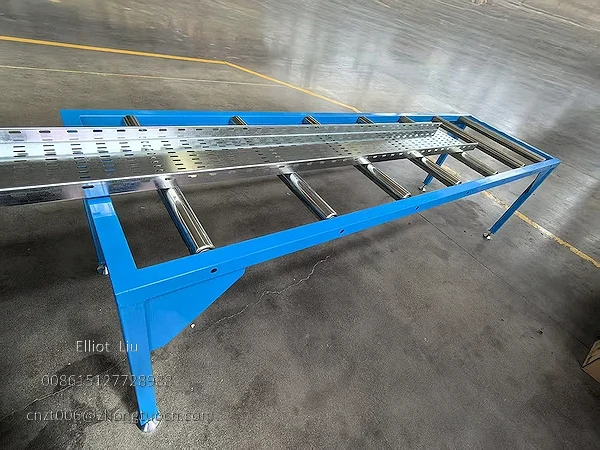
Customers should prepare:
Material type, thickness, and product drawings
Hole pattern, spacing, and punching position
Finished dimensions and planned output
Burr and edge acceptance requirements
Confirm with the supplier:
Punching method, unit configuration, and tonnage
Punch and die clearance and edge maintenance
Burr inspection and acceptance standard
If you are also considering a perforated cable tray roll forming machine, include the hole pattern and burr requirements in your inquiry.
For an auto wire mesh cable tray making machine, the production process differs, so confirm the punching configuration separately.
For this cable tray machine, if the order material or thickness differs from the current reference configuration, explain it during inquiry so the die and punching unit can be checked.
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.