METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
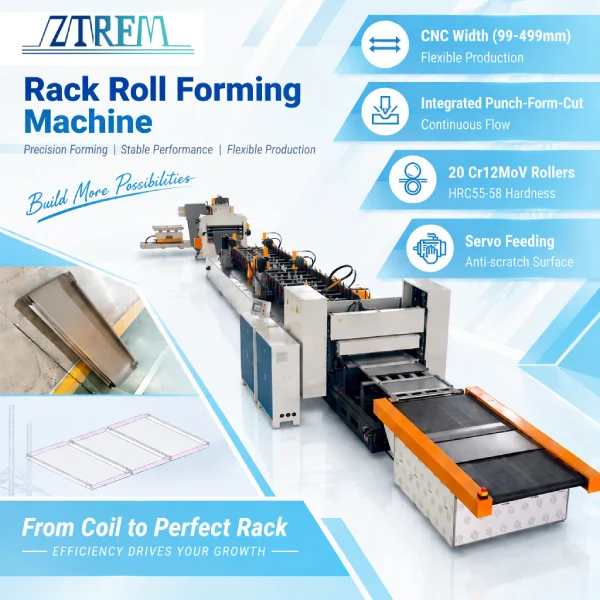
‹ › Rack shelf panels look simple. A flat plate with two flanged edges, plus notches and small holes at the corners. Yet buyers of a warehouse rack forming machine ask about roller material, spindle machining and how well the frame and slideways are fitted long before they ask about tonnage or paint. Those details…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
Rack shelf panels look simple. A flat plate with two flanged edges, plus notches and small holes at the corners. Yet buyers of a warehouse rack forming machine ask about roller material, spindle machining and how well the frame and slideways are fitted long before they ask about tonnage or paint.
Those details decide whether the roll positions hold over years of running.
Roller material and heat treatment set wear life.
Rollers on a warehouse rack forming machine meet the strip first and show profile wear first. This build uses Cr12MoV rollers, vacuum heat treated and tempered twice, at HRC55 to 58. Vacuum treatment and double tempering limit oxidation and decarburisation and relieve stress from the treatment. That makes the roller set a defined part, so roller specs can be compared across suppliers before an order. How long a set lasts also depends on pass design, strip grade and line setup, so hardness alone won't answer it.
Side plates and slideways locate the forming rolls.
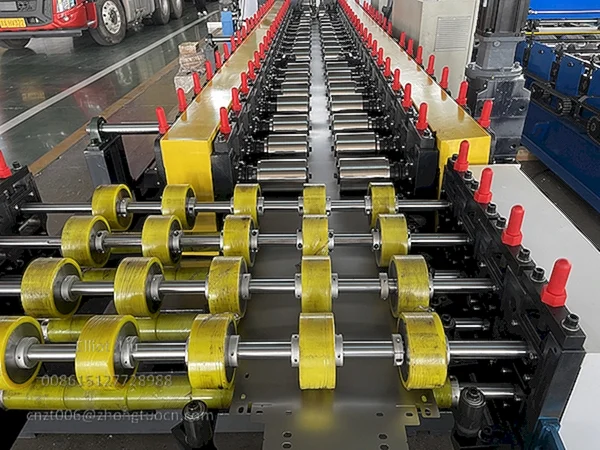
Roll assemblies are positioned by both, so machining quality there sets the base for alignment at assembly and the reference for service later. Main and auxiliary side plates are ground on all six faces, which gives flat and square reference surfaces. Slideways are machined on a machining centre and then bored, producing the guide form and the bore positions that locate each roll assembly. Ground faces can be measured again at service instead of judged by eye.
Spindle and drive carry the running load.
The spindle is 50mm in diameter, made of 45# steel. It's rough machined, quenched and tempered, finish turned, then ground. Quenching and tempering is heat treatment that improves mechanical properties and prepares the steel for later machining and load. Finish turning and grinding hold journal size and surface quality, so the shaft fits its bearings and roll rings. Grinding won't make the steel stiffer, and the two stages serve different purposes. On a warehouse rack forming machine of this build, the parts that carry load can be checked against the duty you plan to run.
Power reaches the main wheel through gear transmission, and the forming rollers are driven by gears as well. The drive side carries two sets of tapered roller bearings, the operator side one set of cylindrical roller bearings. Tapered bearings accept radial and axial load together, cylindrical ones take radial load.
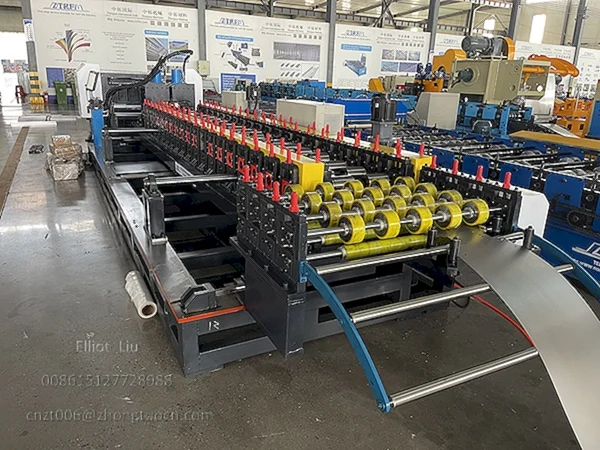
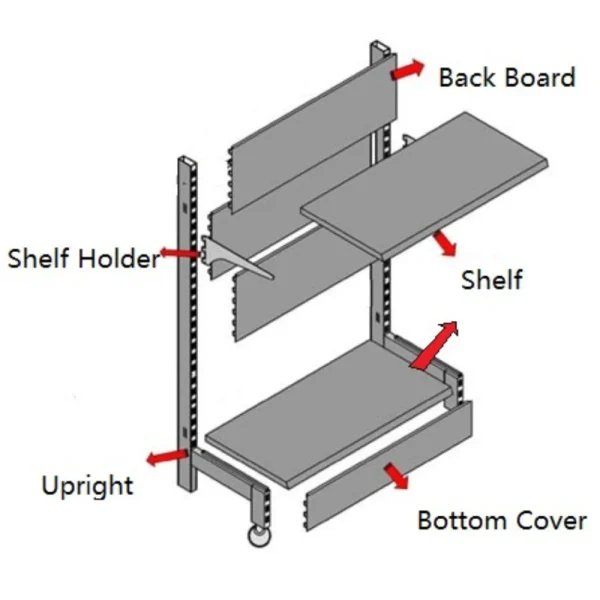
The product is a rack shelf panel, a flat plate with two flanged edges plus notches and small holes at the four corners. This warehouse rack forming machine is built around that single part, so the panel shape defines what the line has to deliver.
It sits between rack beams and carries the goods, so load moves from panel to beam to upright.
Rack makers and builders of warehouse logistics equipment both specify this type of shelf panels machine. Three things matter on every panel. Equal length, straight edges and a flat face.
Length and flanging are both set at the last stage, and the structure there decides whether the two movements stay inside a workable range. One combined die set cuts and flanges in a single step rather than two.
Two linear guides sit under the die frame, each fitted with two sliders, so the frame travels on four. A cylinder returns the frame, and a pin moved by a cylinder fixes the cut length. The hydraulic system includes an unloading function. On a warehouse rack forming machine, this stage is where panel length is settled, so the guides and the pin are the parts to ask about.
Repeat accuracy still depends on guide clearance, pin design and pressure settings.
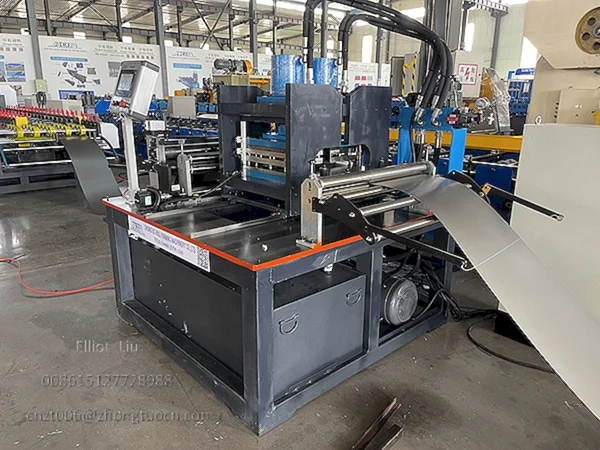
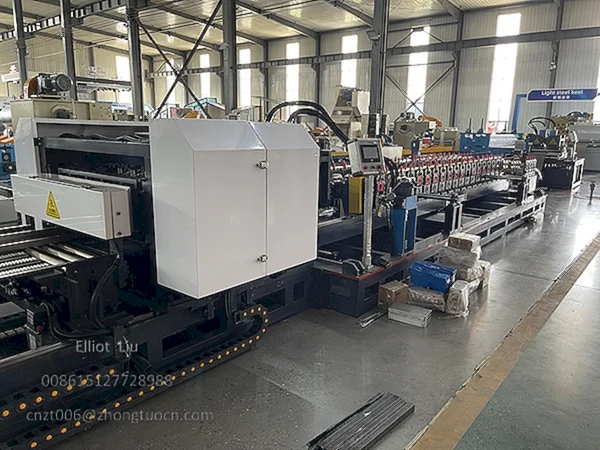
Below are the figures this warehouse rack forming machine is built to.
| Item | Parameter | Specification |
|---|---|---|
| Raw material | Material | Q235 steel coil |
| Thickness | Material thickness | 0.5 to 1.0mm |
| Coil inner diameter | Inner diameter | 450 to 500mm |
| Coil outer diameter | Outer diameter | 1200mm |
| Forming width | Width range, CNC adjustable | 99 to 499mm |
| Forming rollers | Quantity | 20 sets |
| Material | Cr12MoV | |
| Heat treatment | Vacuum heat treated, tempered twice | |
| Hardness | HRC55 to 58 | |
| Forming speed | Line speed, stop and cut time not included | 8 to 10m/min |
| Servo feed | Motor | Huichuan servo motor, 1.3kW |
| Feeding speed | 15 to 30m/min | |
| Pinch rollers | High frequency treatment and hard chrome | |
| Tolerance | Length under 1000mm | plus or minus 0.5mm |
| Spindle | Diameter | 50mm |
| Material | 45# steel | |
| Machining | Quenched and tempered, finish turned and ground | |
| Main motor | Power, variable frequency control | about 15kW |
| Total power | Line total | within 30kW |
| Cutting and flanging | Method | Hydraulic tracking cut and flange |
| Die set | One combined die set | |
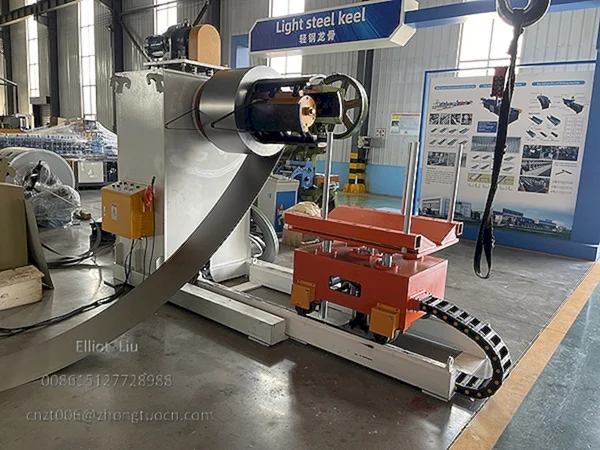
| Decoiler | Capacity | 5T |
| Coil inner diameter | 450 to 500mm | |
| Tensioning | Hydraulic | |
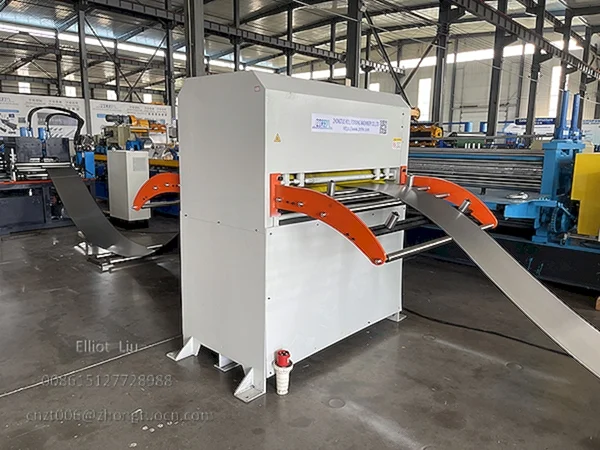
| Leveler | Rollers | 7 rollers, 3 upper and 4 lower |
| Pinch rollers | 2 sets | |
| Control | PLC | Mitsubishi |
| Servo | Huichuan | |
| Inverter | Sine | |
| Relays | IDEC |
Forming speed is the strip speed through the forming section, servo feed speed is the speed of the feed unit. They're separate figures and shouldn't be compared directly.
Forming width adjusts through CNC across 99 to 499mm, and profile follows your drawing. When width changes, the dies that punch the ear and the notch have to be changed as well. They don't follow the setting on their own, so a new panel size is a scheduling matter rather than a surprise. On a warehouse rack forming machine, that's the one item to build into a changeover plan.
Send your panel drawing and specifications, and we'll come back with the arrangement that fits.
We put roller material, heat treatment, side plate machining, spindle process and die structure on one page, because that's what tells you how a warehouse rack forming machine will hold up in your plant.
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.