METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
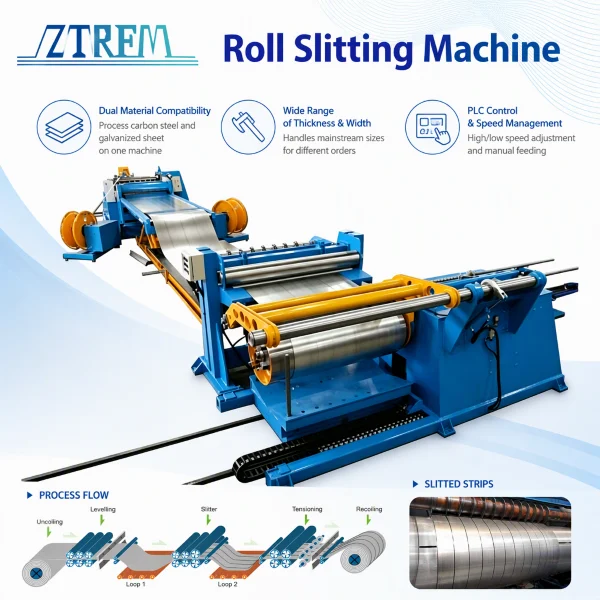
‹ › A roll slitting machine deals with the difference between mill supplied coils and downstream needs. Wide coils come in specific widths, and material conditions vary. Downstream lines have their own requirements for strip width, material type, and cut edge quality. The machine slits wide coils lengthwise into narrow strips that meet those requirements. This equipment…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
A roll slitting machine deals with the difference between mill supplied coils and downstream needs. Wide coils come in specific widths, and material conditions vary. Downstream lines have their own requirements for strip width, material type, and cut edge quality. The machine slits wide coils lengthwise into narrow strips that meet those requirements.
This equipment handles carbon steel and galvanized sheet across a range of thickness and width.
Wide coils leave the mill with a fixed width. Downstream stamping dies, tube mills, and roll forming lines each have their own requirements for material type, width, and cut edge quality. A width mismatch can stop material from entering the line directly, and a rough cut edge can speed up die wear.
A roll slitting machine does this conversion. It slits a wide coil lengthwise into multiple narrow strips, with width and cut edge quality controlled to downstream requirements.
Different downstream scenarios have their own focus on material type and width for slit strip:
Automotive stamping: The die sets the feed width. Carbon steel strip that matches the die width feeds more smoothly.
Welded tube production: Continuous welding needs consistent width. Both carbon steel and galvanized sheet work for tube making.
Construction profile processing: Roll forming lines feed at a fixed width. Galvanized strip goes into roof panels and wall panels.
Across these scenarios, incoming width and cut edge quality need to match line conditions.
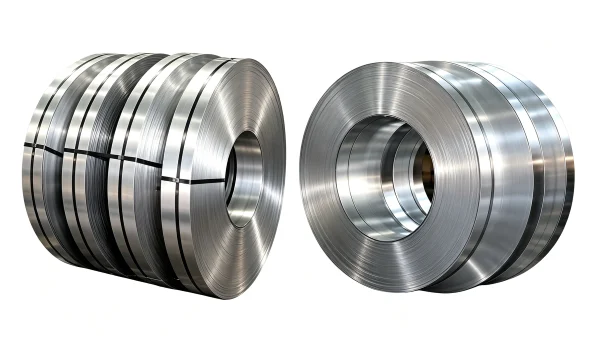
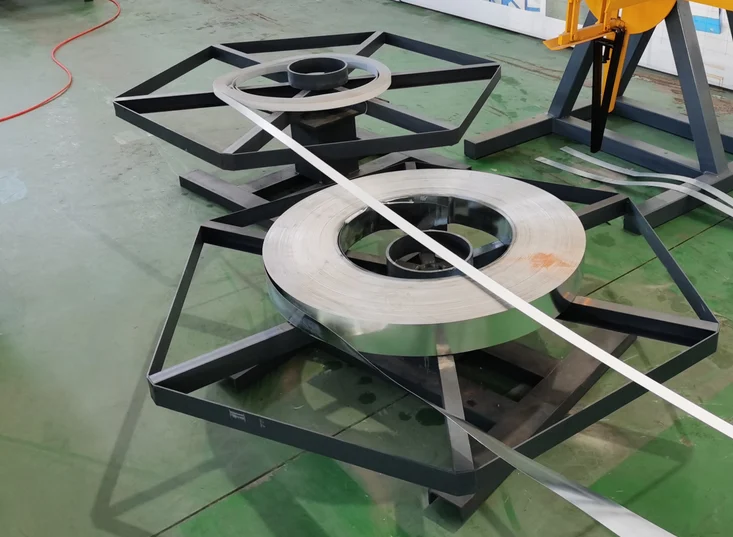
Carbon steel and galvanized sheet behave differently during slitting. Carbon steel surface condition depends on rolling and surface treatment, while galvanized sheet has a zinc layer that slitting should avoid damaging.
This sheet metal slit machine handles both carbon steel and galvanized sheet. Blade material is H13K, and shaft material is 40Cr. Blade material and gap settings match the material.
Blade gap is a key variable for slit quality. A larger gap can affect burr formation, and a smaller gap can speed up blade wear. Thick and thin sheet need different gaps, so settings depend on material thickness, blade condition, and process conditions. The goal is to control burr and edge quality.
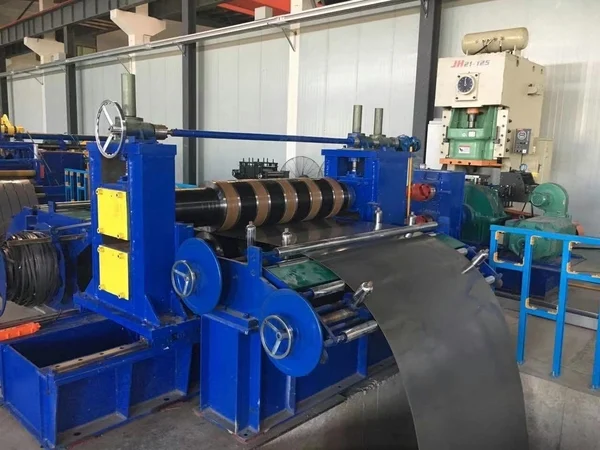
This slitting steel machine brings the following value in material and size adaptability:
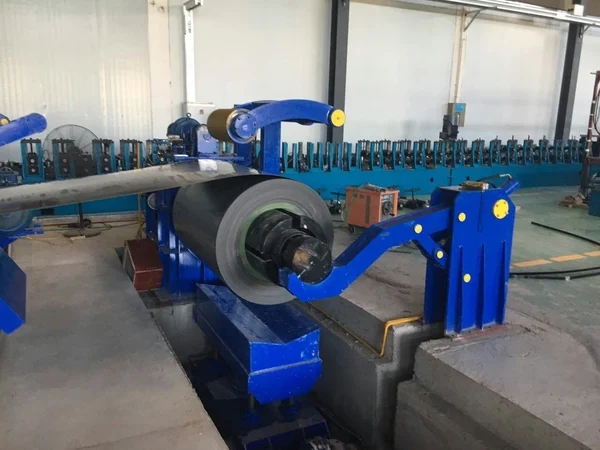
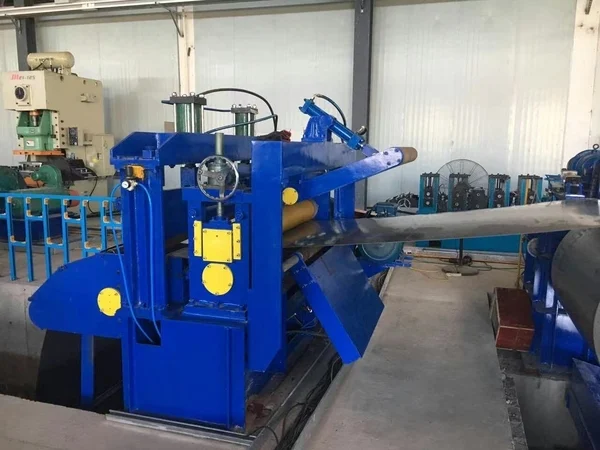
| Parameter | Specification |
|---|---|
| Production line length | 23 meters |
| Production line width | 8 meters |
| Material thickness range | 0.3mm to 3.5mm |
| Material width range | 500mm to 1600mm |
| Maximum coil outer diameter | 1600mm |
| Maximum coil weight | 15 tons |
| Slitting width accuracy | ±0.05mm |
| Line direction | Right to left |
| Operators required | 1 mechanical engineer and 2 common workers |
The parameters above describe this roll slitting machine.
On a roll slitting machine, thin and thick sheet show different cut edge behavior. Thin sheet has lower stiffness, so edge stability is harder to control and gap settings need more care. Thick sheet needs higher shear force, blade wear is faster, and burr control depends more on blade condition and gap settings.
On a roll slitting machine, carbon steel and galvanized sheet also differ in cut edge requirements. Carbon steel mainly looks at burr and edge flatness. Galvanized sheet also needs attention to whether the zinc layer is scratched or peeled. As blades wear, burr can grow and cut edge quality drops. Operators check blade condition based on the cut edge and decide whether to adjust the gap or change blades.
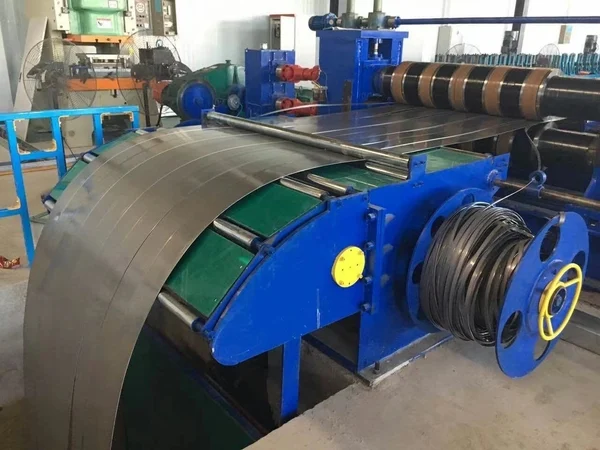
When changing width on a roll slitting machine, adjust the side guide device. The adjustment range is 500mm to 1600mm, driven by a motor and screw. After adjustment, check that the strip enters the slitter centered.
On a sheet metal slit machine, thickness changes need attention to blade gap and tension settings. When moving from thick to thin sheet, reduce the gap. When moving from thin to thick sheet, increase the gap.
After a spec change on a roll slitting machine, cut a test strip and check cut edge quality and recoiling condition, then run continuous production.
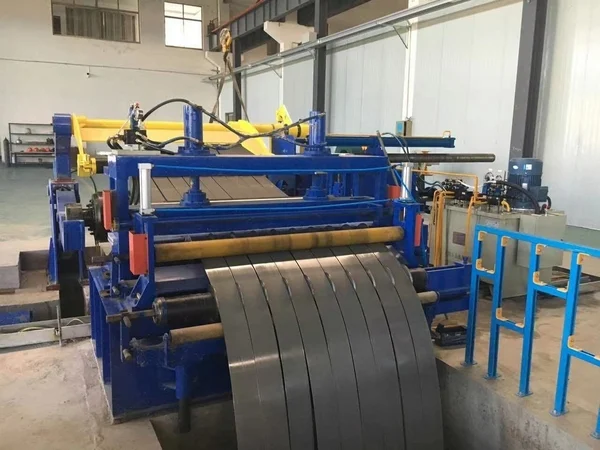
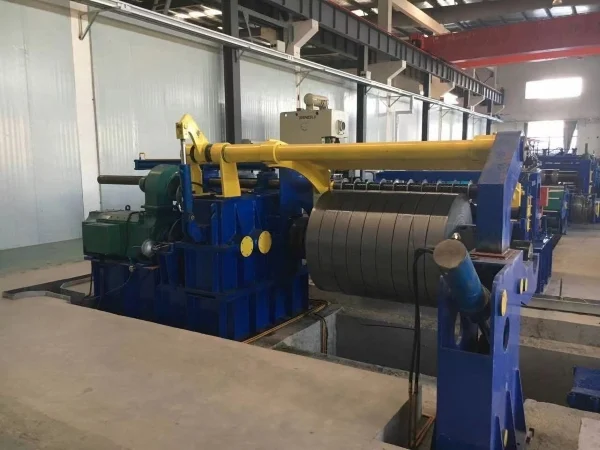
Material type, thickness, width, and blade gap settings all affect slitting results. The value of a roll slitting machine is not in the numbers on a parameter table, but in whether the slit strips go directly into downstream lines.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.