METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
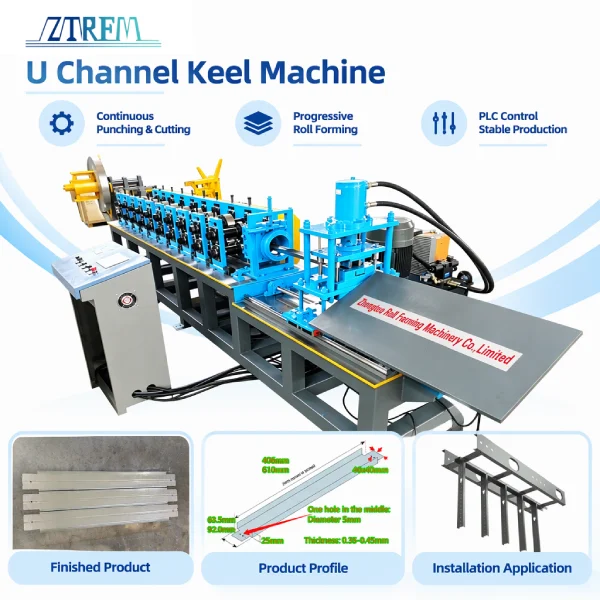
‹ › On a light steel framing job, the crew needs a reliable connector between parallel joists before the wall goes up. That connector starts as galvanized coil on a u channel keel machine. The line takes the coil through decoiling, progressive forming, punching and shearing, and receiving. The finished profile serves parallel framing connections and…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
On a light steel framing job, the crew needs a reliable connector between parallel joists before the wall goes up. That connector starts as galvanized coil on a u channel keel machine. The line takes the coil through decoiling, progressive forming, punching and shearing, and receiving.
The finished profile serves parallel framing connections and top fixing for interior nonstructural walls. The machine combines a manual decoiler, a forming section with 12 rollers, a punching and shearing unit controlled by PLC, a hydraulic station, and a manual receiving table.
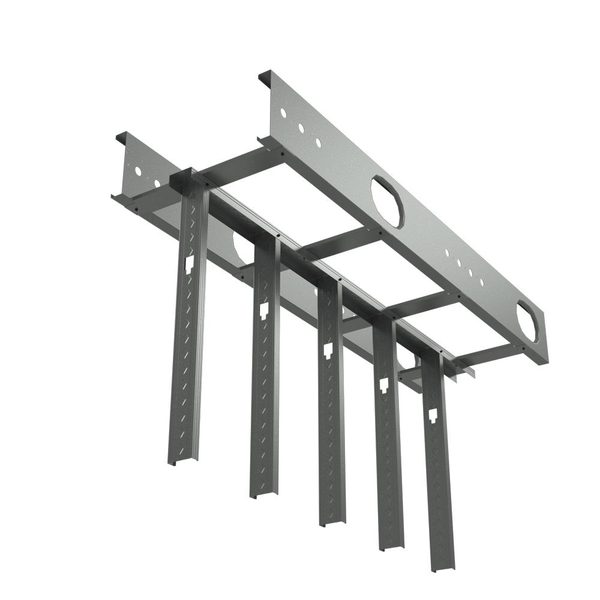
A framing crew usually needs a connector between parallel joists before the wall goes up. U shaped keel profiles from a u channel keel machine fill that role. The profile sits between parallel members, and connectors pass through holes to fix it to brackets or members. This keeps spacing and stability during installation and use.
Top fixing for interior nonstructural walls is another use. The wall top connects to the upper structure through the profile and connectors. Different projects set different finished size and hole layout requirements, so the profile must match the drawing.
Continuous punching and shearing follow the production pace. Stopping for every punch and cut slows the line. This u channel keel machine completes both while material keeps moving. A tracking unit controlled by PLC, a hydraulic station, and blades made of Cr12 and quenched support the process.
Forming completes in steps and suits continuous production. The forming section uses twelve rollers, and each roller takes a smaller share of deformation. The strip bends step by step into the target section.
Power delivery stays matched to continuous forming. A reducer motor and gear transmission carry power from the motor to each roller, so the drive setup works with continuous forming.
Key part materials match their tasks. GCr12 rollers handle forming, tempered steel shafts carry torque, and blades made of Cr12 and quenched handle shearing.

At the front of the line sits a manual decoiler. It holds a 2.5 ton coil, takes 450 to 550 mm inner diameter, and runs 300 mm uncooling width. The decoiler does not drive the strip. The forming system pulls it forward, so the coil turns passively as the line runs.
An entry guide table then helps the strip enter the forming section in a neat, parallel, and uniform way. This unit sets the strip condition as it enters the forming section.

The main unit uses a memorial arch frame and a welded square tube structure. The forming section has 12 rollers, GCr12 roller material, shafts made of 45# steel and tempered at φ50 mm, gear transmission, and a 5.5 kW main motor. The main unit measures about 5500 × 1500 × 1500 mm.
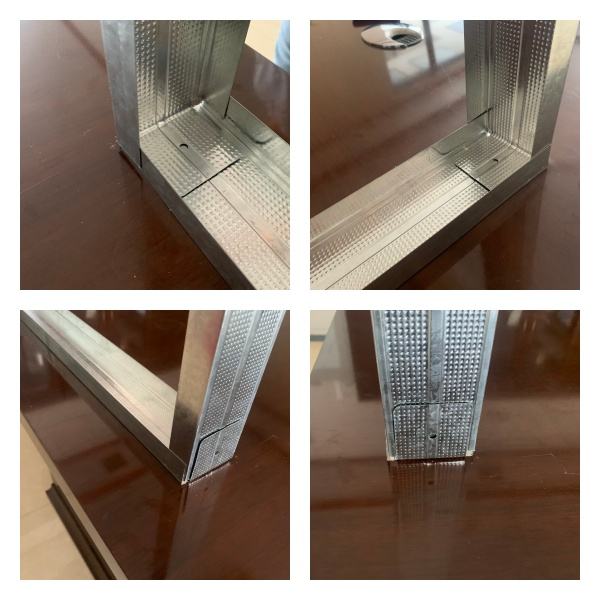
Roller surfaces go through polishing, hard plating, and heat treatment. Roller spacers between stations adjust profile size, and the operation video shows the adjustment method. The knurl pattern sits on the web and does not cover the whole panel.
Punching and shearing run on an automatic tracking system controlled by PLC. The station follows forming speed and completes punching and cut to length while material keeps moving.
The set includes blades, a hydraulic tank, and a cutter with a servo motor. The hydraulic station provides power, and blades use Cr12 with quenching.
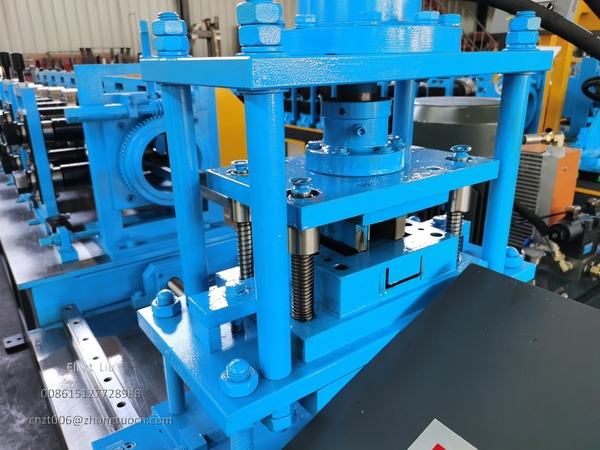
A control computer coordinates forming, punching and shearing, and receiving. Finished profiles leave the shear station and go to a manual receiving table for piece by piece collection.
The complete line includes a decoiler, forming section, punching and shearing system, hydraulic station, control computer, and receiving table.
The table below lists the main parameters of this u channel keel machine.
| Parameter | Specification |
|---|---|
| Raw material | Galvanized steel coil |
| Material thickness | 0.35 to 0.45 mm |
| Finished width options | 63.5 mm / 92 mm |
| Finished length options | 406 mm / 610 mm |
| Main motor power | 5.5 kW |
| Power supply | 480V / 60Hz / 3 phase |
| Working speed | 0 to 15 m/min with punching and shearing |
| Number of rollers | 12 |
| Roller material | GCr12 |
| Shaft material | 45# steel, tempered |
| Shaft diameter | φ50 mm |
| Frame type | Memorial arch |
| Frame structure | Welded square tube structure |
| Transmission type | Gear transmission |
| Blade material | Cr12, quenched |
| Machine weight | About 5.5 tons |
| Working space | About 12m × 2.0m × 1.5m |
| Main unit size | About 5500 × 1500 × 1500 mm |
| Decoiler capacity | 2.5 tons |
| Decoiler inner diameter | 450 to 550 mm |
| Uncooling width | 300 mm |
Working speed covers the run with punching and shearing. Working space means the space needed for machine layout, and main unit size means the outer size of the main unit.
When the crate opens, the buyer gets one maintenance tool set, three spare gears, and one operation manual. The manual covers installation, parameter setup, daily operation, maintenance, and troubleshooting.
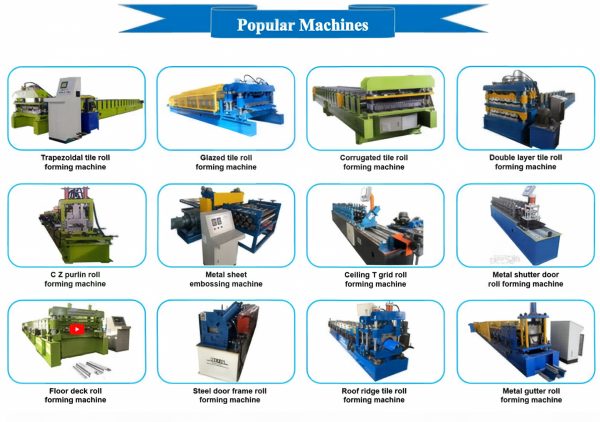
The same supplier also offers related cold roll forming machines for u channel roll forming machine buyers:
Ceiling system roll forming machine
Door system forming machine
What do I get besides the machine itself?
You get one maintenance tool set, three spare gears, and one operation manual. The manual covers installation, setup, operation, maintenance, and troubleshooting.
What coil thickness and finished sizes can this line handle?
It handles galvanized steel coil from 0.35 to 0.45 mm. Finished width options are 63.5 mm and 92 mm, and finished length options are 406 mm and 610 mm.
How do we change the profile size?
Roller spacers between stations adjust profile size. The operation video shows the adjustment method, and the exact range needs confirmation against the finished product.
What does the punching and shearing set include?
One blade set, one hydraulic tank, and one cutter with a servo motor. Blades use Cr12 with quenching.
Where does the knurl pattern sit?
On the web, not the whole panel. This keeps the edges flat for connectors.
Each quotation reflects one configuration, and each u channel keel machine is a custom setup. Parameters are not fixed. Material thickness, finished width and length, production speed, voltage, floor space, and profile can be discussed with the professional team. The exact range and requirements need confirmation.
Share your drawing or sample, and the team will discuss the configuration for your line.
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.