METAL ROLL FORMING MACHINE
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
Zhongtuo roll forming Systems is a "one-stop shop" for all your roll forming needs,enabling our customers to save time and money when buying roll forming machines,to help customers grow.
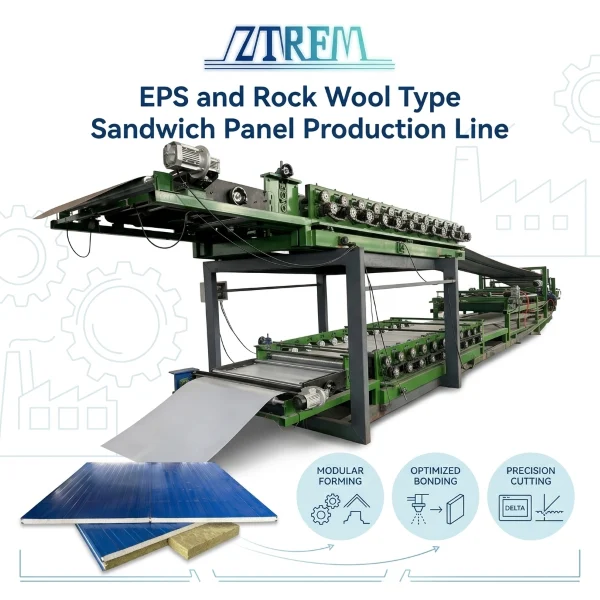
‹ › One EPS and rock wool type sandwich panel production line can run roof and wall panels through decoiling, forming, laminating, cutting and output. Compatibility describes product scope. It does not mean switching costs nothing. For the EPS and rock wool type sandwich panel production line, the composite machine, glue system, heating system and control system provide…
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Detailed Content
One EPS and rock wool type sandwich panel production line can run roof and wall panels through decoiling, forming, laminating, cutting and output. Compatibility describes product scope. It does not mean switching costs nothing.
For the EPS and rock wool type sandwich panel production line, the composite machine, glue system, heating system and control system provide process conditions for different cores. They do not remove process differences between EPS and rock wool. Confirm product scope, machine setup, switching flow and acceptance terms in the technical agreement.
This EPS and rock wool type sandwich panel production line covers roof and wall panels with EPS and rock wool cores.
Roof and wall panels on one line: roof top sheets use trapezoidal profiles, wall panels use their own profiles, and both sheets are formed by roll forming machines. Single and double layer forming keep bottom and top sheets off the same rollers.
Switching between EPS and rock wool: both cores share panel applications, but need different gaps, pressure and glue wetting. Confirm composite conditions, glue and heating when orders switch.
Multiple profiles and cores: switch frequency depends on profile count, panel length and order sequence. Grouping similar profiles can cut changeovers.
The current line has 12+12+17 forming stations. Discuss station count and roller setup around your profile mix.
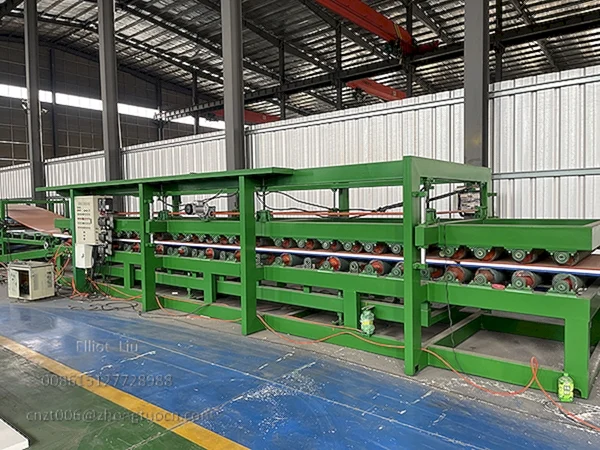
For the EPS and rock wool type sandwich panel production line, the current setup includes 3 manual 5 ton decoilers, single and double layer roll forming machines, a composite machine, glue system, heating system, PLC control stations, a flying saw and collecting tables.
Forming split: single and double layer forming handle bottom and top sheets, so roof trapezoidal top sheets and wall bottom sheets do not share one roller set. Station count can follow the profile mix; the current setup has 12+12+17 stations.
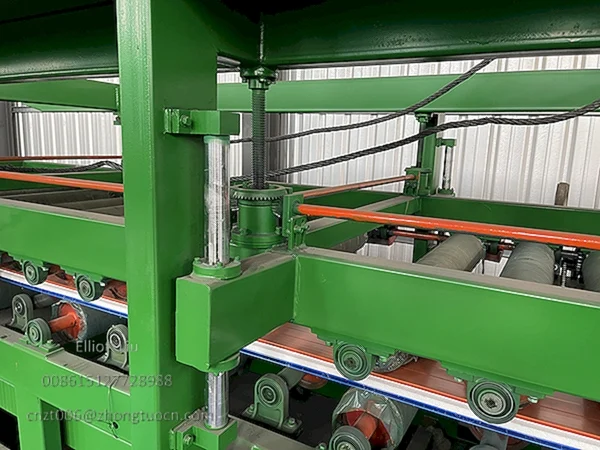
Glue and heat: the composite machine has glue spray or drip and infrared heating for glue application and curing. Settings need trial runs by core and glue type.
Batch cutting control: Delta PLC and touch screen set cut length and quantity, and the flying saw cuts on the run. The value is batch setup and count management; tolerance and cut section need trial checks.
The current 2 glue systems, 1 heating system and 2 control stations are this setup's reference. They are not fixed for every compatible line.
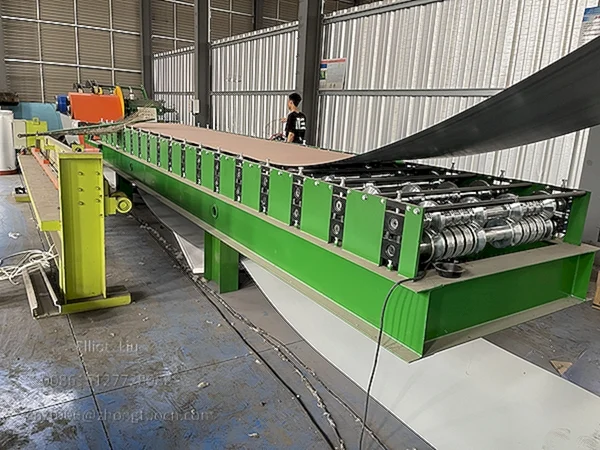
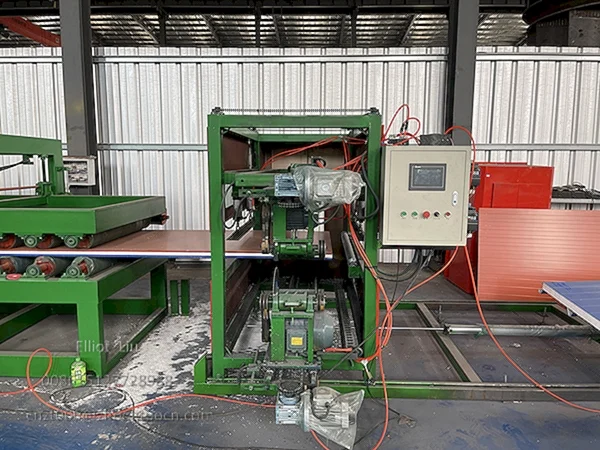
The table below lists main parameters of the EPS and rock wool type sandwich panel production line. It shows the current reference setup, not every setup of this machine type.
Speed, profile, voltage, color, line layout and section positions can be discussed around your requirements. Confirm them in the technical agreement and final layout drawing.
| Accessory name | Parameter name | Parameter |
|---|---|---|
| Whole line | Core materials | EPS, rock wool |
| Panel applications | Roof panels, wall panels | |
| Total power | 32kW | |
| Working voltage | 380V 50Hz 3P, customizable | |
| Line speed | about 0-6 m/minute | |
| Product width | 1000mm, 1200mm | |
| Product thickness | 50-250mm | |
| Annual output | 600,000 square meters, based on annual working days, daily working hours and products | |
| Working dimensions | 45m x 4m x 7m | |
| Machine weight | About 10 tons | |
| Decoiler | Quantity | 3 sets |
| Capacity per unit | 5 tons | |
| Type | Manual | |
| Use | 1 for bottom sheet, 2 for top sheet | |
| Roll forming machine | Configuration | 1 set single layer plus 1 set double layer |
| Current forming stations | 12+12+17 stations | |
| Composite machine | Function | Glue spray or drip, infrared heating, pressing |
| Current driving stations | 55 stations | |
| Rubber driving roller diameter | 180mm | |
| Glue system | Quantity | 2 sets |
| Heating system | Quantity | 1 set |
| Control system | Brand | Delta PLC plus touch screen |
| Control station quantity | 2 sets | |
| Cutting system | Type | Flying saw |
| Function | Set cut length and quantity | |
| Collecting table | Quantity | 2 sets |
| Type | Manual | |
| Length | 3m |
For this setup, the table is a starting point for technical clarification. The 55 driving stations, 12+12+17 stations, 2 glue systems and 2 control stations belong to this setup and do not apply to every compatible line.
When you ask for a quote, share your profile mix, core ratio, panel length range and factory conditions so the supplier can explain setup changes.
For the EPS and rock wool type sandwich panel production line, compatibility answers whether the line can produce. Changeover management answers whether it can produce steadily after the switch. Going from EPS to rock wool, or from wall panels to roof panels, means checking composite settings, glue and heating, cutting parameters and first piece approval. Confirm switch time, adjustment steps and waste ratio in the technical agreement and trial run.
The composite machine has 55 driving stations and 180mm rubber driving rollers for pressing and driving. Pressure and gap still need trial checks by core, profile and glue type. Do not read this as automatic adjustment for every core or no adjustment at all.
First piece approval checks bond, panel surface, cut length and profile fit. Sort waste by core and profile. Rock wool dust and edge trim should not mix with EPS waste.
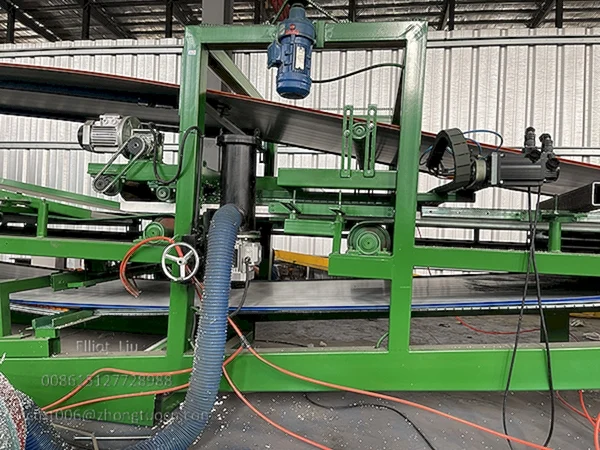
Grouping orders with the same core and similar profiles can reduce changes. When profiles differ a lot, profile parts and first piece checks also differ.
Before a switch, confirm core, glue, profile parts and cutting parameters. During the switch, watch composite gap, heating and first piece condition. After the switch, complete first piece approval and waste sorting. Operator training should cover core identification, process settings and first piece checks. Process management for a core switch is not automatic. Follow the technical agreement and trial results.
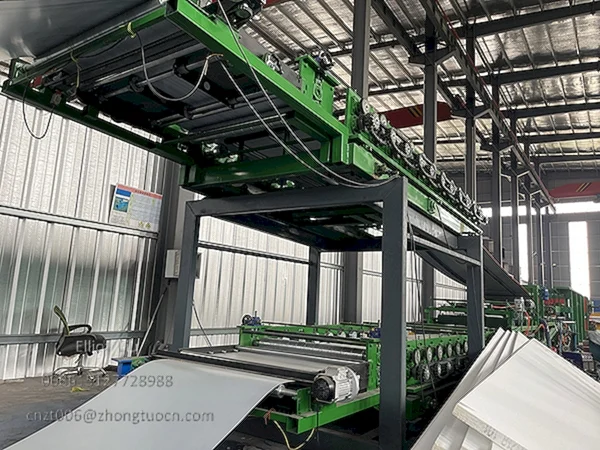
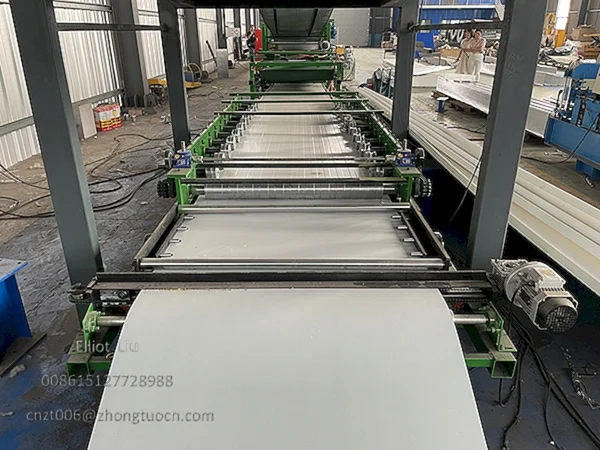
Before you buy the EPS and rock wool type sandwich panel production line, put product scope, machine setup, changeover acceptance and factory layout into the technical agreement. Do not stop at a yes or no answer on EPS and rock wool.
Product scope: confirm core types, panel types, thickness, width and length ranges, plus roof trapezoidal profiles and wall panel joint forms. Trapezoidal profiles can be customized to your drawings.
Machine setup: confirm forming stations, composite machine, glue and heating systems, flying saw and control system. The current 12+12+17 stations, 55 driving stations and 2 glue systems are this setup's reference, not a fixed setup.
Changeover and acceptance: the agreement should cover switch items, first piece approval, cut settings and waste responsibility. Do not promise switch time or waste ratio without trial evidence. Check acceptance targets in a product trial.
Factory layout: confirm factory conditions, machine dimensions and the final layout drawing. Layout, output direction, voltage system and color can be customized to factory conditions. The supplier should confirm whether the factory and machine match on the layout drawing. Do not assume a new layout will solve every space problem.
For the EPS and rock wool type sandwich panel production line, clear boundaries turn compatibility into acceptable production conditions.
Contact: Elliot liu
Email: [email protected]
WhatsApp: 008615127728988
Contact Us For More Roll Forming Machine Detailed Information
You can contact us either through phone number 0086-15127728988 within our working hours, or send an email to [email protected], or send an inquiry form to us using "Inquiry Now" option. Our customer representatives will respond as soon as possible.